Guided Entry
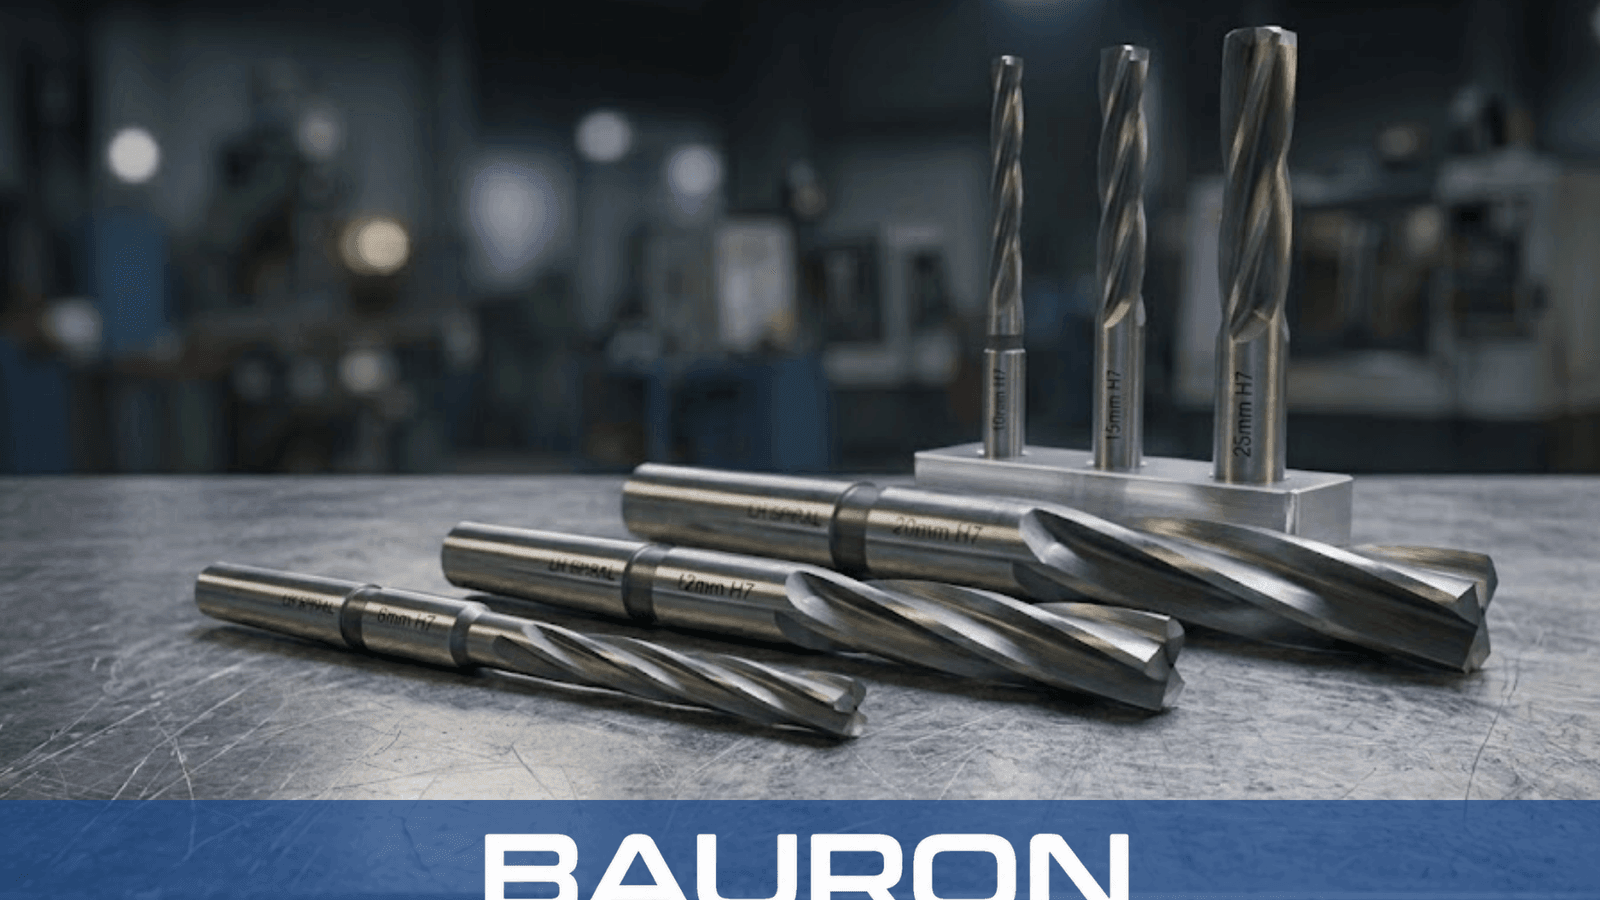
A chamfered tip guides the tool into the pre-drilled hole.
Rotate the model with a mouse or one finger. Use the mouse wheel or a two-finger gesture for controlled zoom.
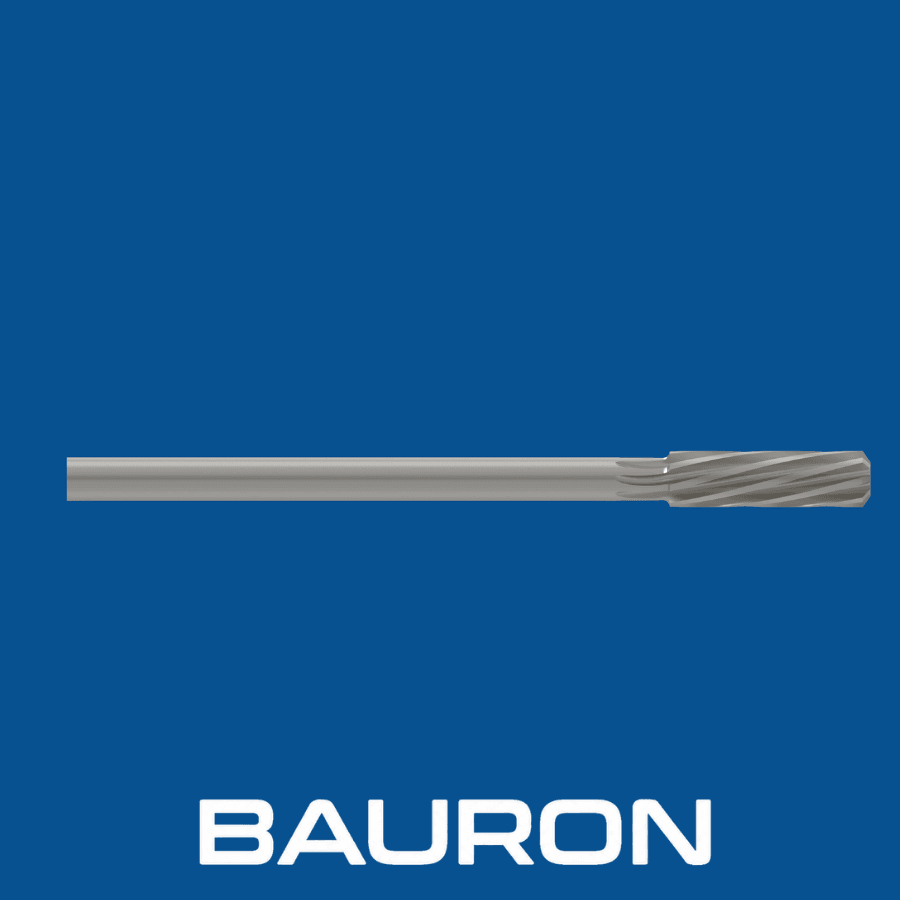
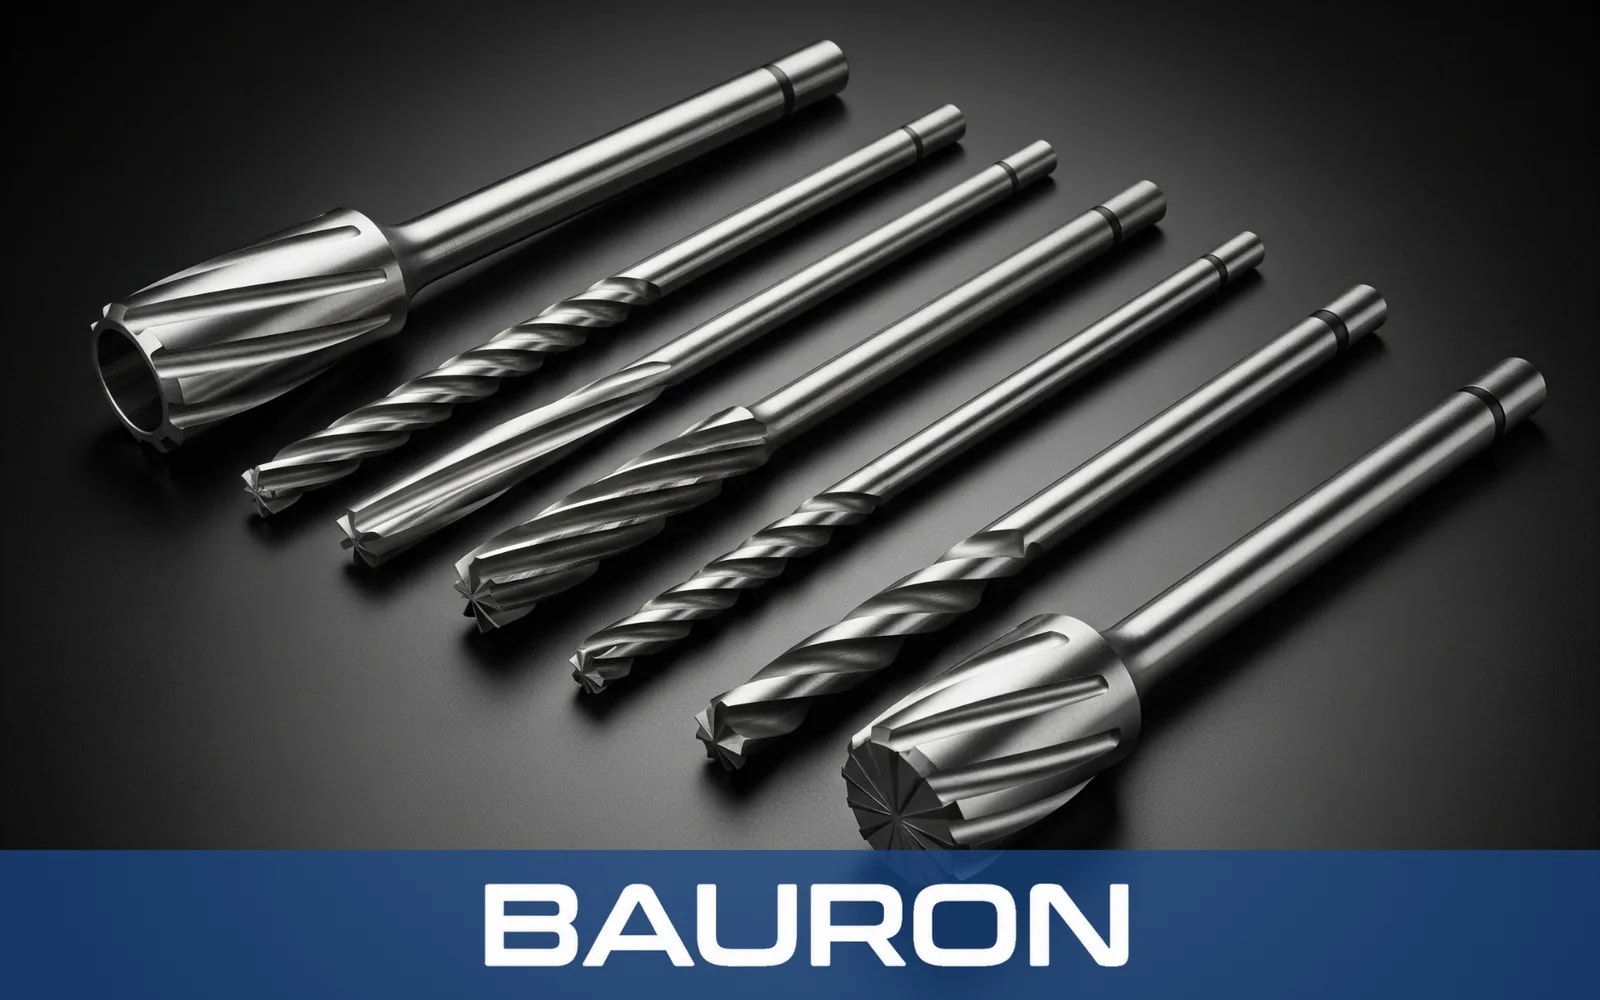
A left-hand spiral reamer sizes through-holes, including work in materials prone to grabbing. Its left-hand spiral and right-hand cut support controlled finishing by pushing chips ahead of the tool and resisting aggressive self-feeding.
A chamfered tip guides the tool into the pre-drilled hole.
Right-hand rotation progressively shears material from the inner walls.
Left-hand spiral flutes push chips ahead of the tool, making this the through-hole version of the spiral flute reamer.
Continuous shearing supports a smooth, precise internal diameter.
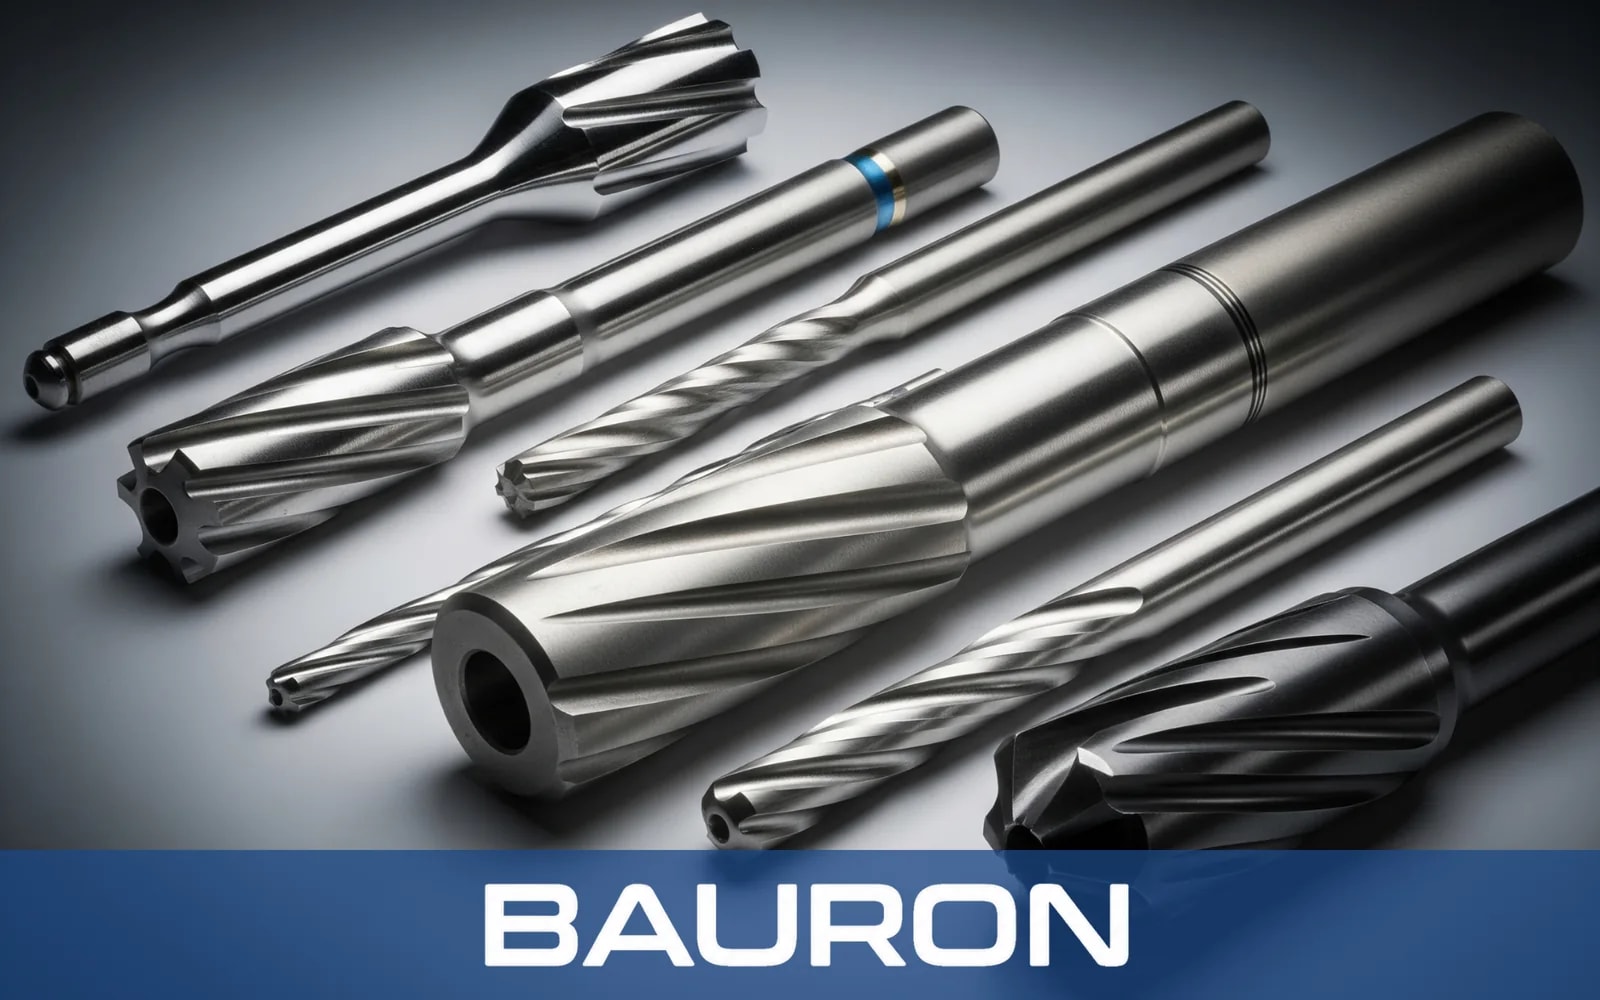
A left-hand drill reamer spiral pushes chips forward to help protect the finished surface from scratching.
Works with standard clockwise spindle rotation.
Helps prevent self-feeding or grabbing into the workpiece.
Distribute cutting forces around the bore to support accuracy and reduced chatter. Flute spacing options are covered in the Reamers Design guide.
Support tight dimensional tolerances and a fine surface finish.
Supports secure clamping in CNC chucks or hand-reaming wrenches.
| Specification | Range / Details |
|---|---|
| Diameter Range | 1/16" to 2"; standard and metric sizes available |
| Flute Geometry | Left-hand spiral, right-hand cut |
| Number of Flutes | 4 to 8, depending on diameter |
| Shank Type | Straight, Morse taper, or square end |
| Tolerance | H7 standard or custom precision-ground |
| Operation Type | Through-holes |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS (High-Speed Steel) | Mild steel, aluminum, and general-purpose through-holes. | An economical option with toughness for standard production. |
| Solid Carbide | High-volume production on abrasive or very hard alloys. | Provides high rigidity and extended wear life. |
| TiCN Coating | Sticky materials such as stainless steel or cast iron. | Reduces friction and helps limit edge buildup. |
HSS provides toughness for general through-hole work, solid carbide supports rigid high-volume machining, and TiCN can reduce friction in sticky or abrasive workpiece materials.
Use rigid holders for automated through-hole finishing.
Support tailstock or turret operations on stationary or rotating cylindrical parts.
Provide controlled vertical reaming with manual or automatic feed.
Drive square-shank versions for controlled hand reaming.
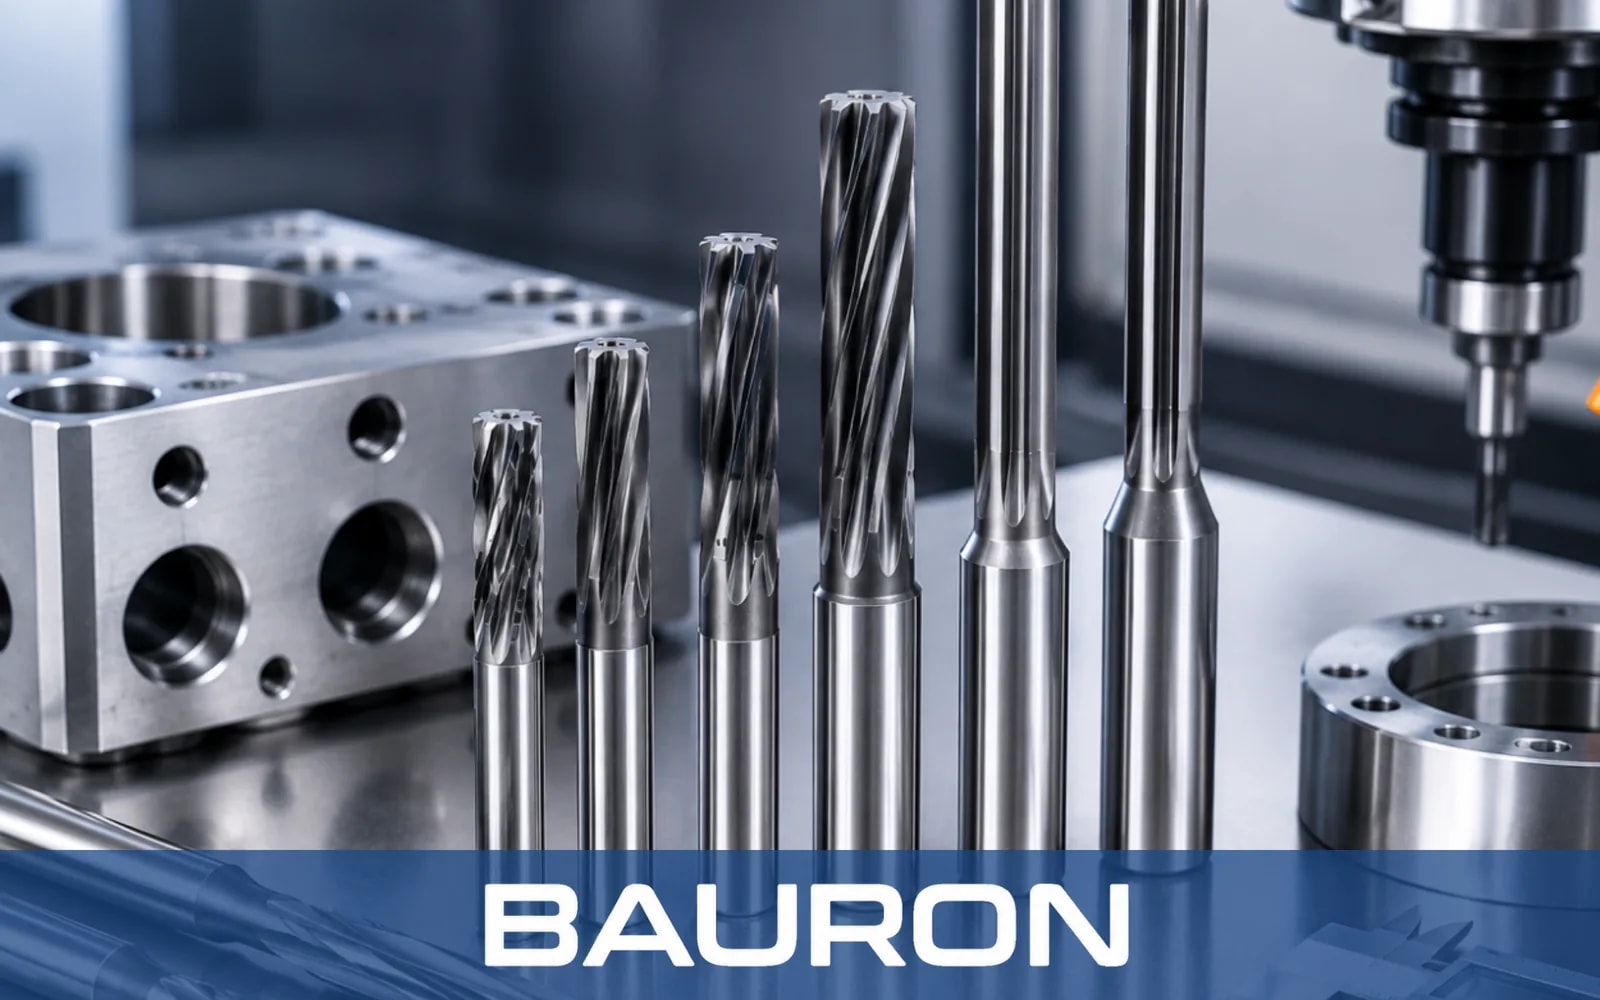
Pushes chips forward to help prevent them from scoring the newly finished bore.
Bridges gaps such as keyways or cross-holes with reduced risk of catching.
The negative axial rake helps limit grabbing in tough alloys that can bind straight-flute reamers, including the heat-resistant superalloys handled in aerospace tooling and machining.
Provides gradual cutting pressure when used as a spiral hand-reaming tool during assembly.
A left-hand spiral reamer pushes chips forward and resists self-feeding, making it suited to interrupted cuts and through-holes. A straight-flute reamer has parallel flutes and is generally used for standard, non-interrupted holes.
It should generally not be used for blind holes because the flute direction pushes chips toward the bottom, where packing can damage the tool, surface, or workpiece. For blind holes, a right-hand spiral reamer draws chips back toward the entrance.
The right-hand cut runs with standard clockwise spindle rotation. The left-hand spiral creates a negative axial rake that resists the feed direction and helps prevent sudden grabbing.
Bauron recommends cobalt HSS or solid carbide. The spiral geometry bridges the interruption, while the harder substrate helps the cutting edges withstand repeated impacts.
Bauron can manufacture custom reamers with specific diameters, shank lengths, tolerances, and coating configurations to match blueprint requirements.
Bauron Precision Tools provides design and engineering support for custom geometries, coatings, diameters, shank lengths, and tolerances. Share the application and blueprint requirements for technical review.
Talk to Engineering