Spindle Mounting
The shank is secured in a CNC collet or chuck; a chuck reamer is built for exactly this kind of mounting.
Rotate the model with a mouse or one finger. Use the mouse wheel or a two-finger gesture for controlled zoom.
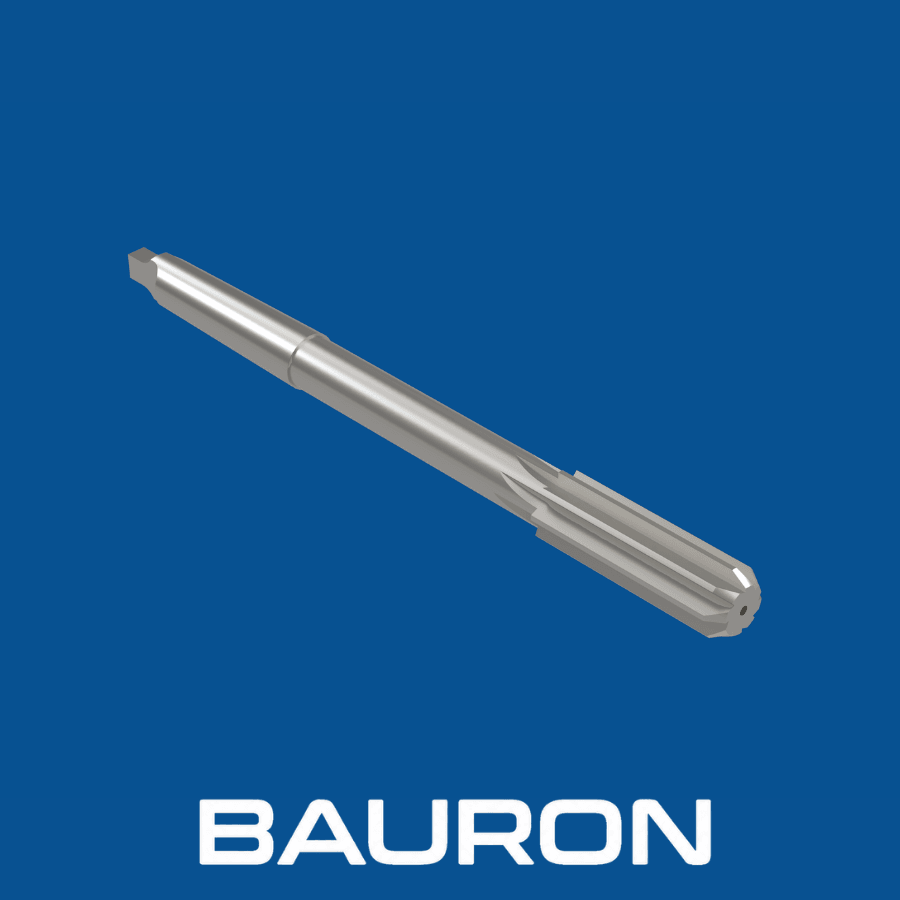
As a reamer manufacturer, Bauron builds machine reamers as finishing tools for rigid, automated setups. They remove a controlled amount of material from a pre-drilled hole to produce tight diametrical tolerances and a fine surface finish during CNC production.
The shank is secured in a CNC collet or chuck; a chuck reamer is built for exactly this kind of mounting.
A chamfered tip guides the cutter into the existing hole.
Rotation and controlled feed allow the flutes to shear material from the bore.
Selected flute geometry carries chips away during the cycle.
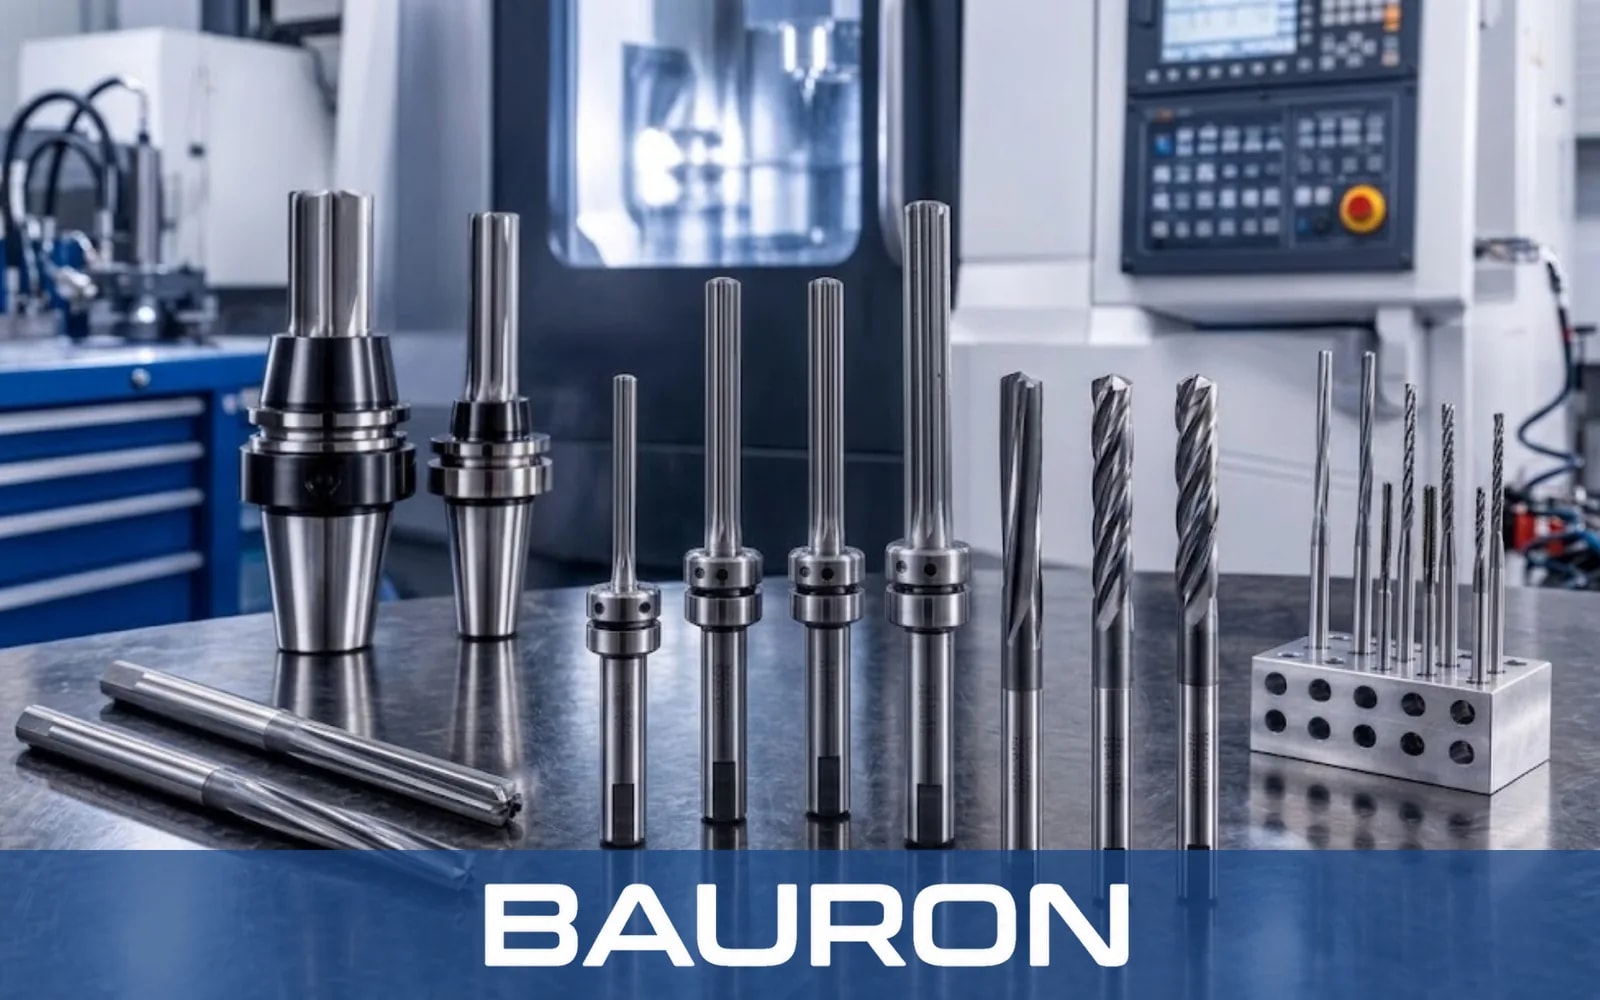
Provides rigidity to help limit chatter in CNC machining centers.
Supports rapid cutting engagement in production cycles.
Support fine surface finishes and close engineering tolerances.
Provide secure mounting in industrial collets and holders; large-diameter shell reamers mount on a separate arbor instead.
Application-specific profiles can be engineered for specialized hole-finishing tasks.
Selected flute geometry helps reduce bore scoring and tool damage during continuous operation.
| Specification | Range / Details |
|---|---|
| Diameter Range | 1/16" to 2"; custom sizes up to 4" available |
| Flute Type | Straight, right-hand spiral, or left-hand spiral |
| Shank Type | Straight, Weldon, or Morse taper |
| Number of Flutes | 4 to 12, depending on tool diameter |
| Tolerance | Precision-ground to standard H7 or custom specifications |
| Format | Solid body or adjustable machine reamer |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| Cobalt (HSS-Co) | High-volume production on tough alloys. | Offers greater heat resistance and edge life than standard HSS. |
| Solid Carbide | Abrasive materials and rigid CNC environments. | Provides high wear resistance and rigidity for close tolerances. |
| TiAlN Coating | Dry machining and high-temperature cutting. | Protects the substrate and can reduce friction. |
Cobalt HSS supports production in tough alloys, solid carbide reamers provide rigidity and wear resistance in stable setups, and TiAlN, a common coating for reaming, can protect the substrate during dry or high-temperature cutting.
Use rigid holders for automated hole finishing.
Mount reamers in turrets to size internal diameters on rotating cylindrical parts.
Integrate reaming into high-volume automated production cycles, where drill reamers can merge drilling and finishing in one tool.
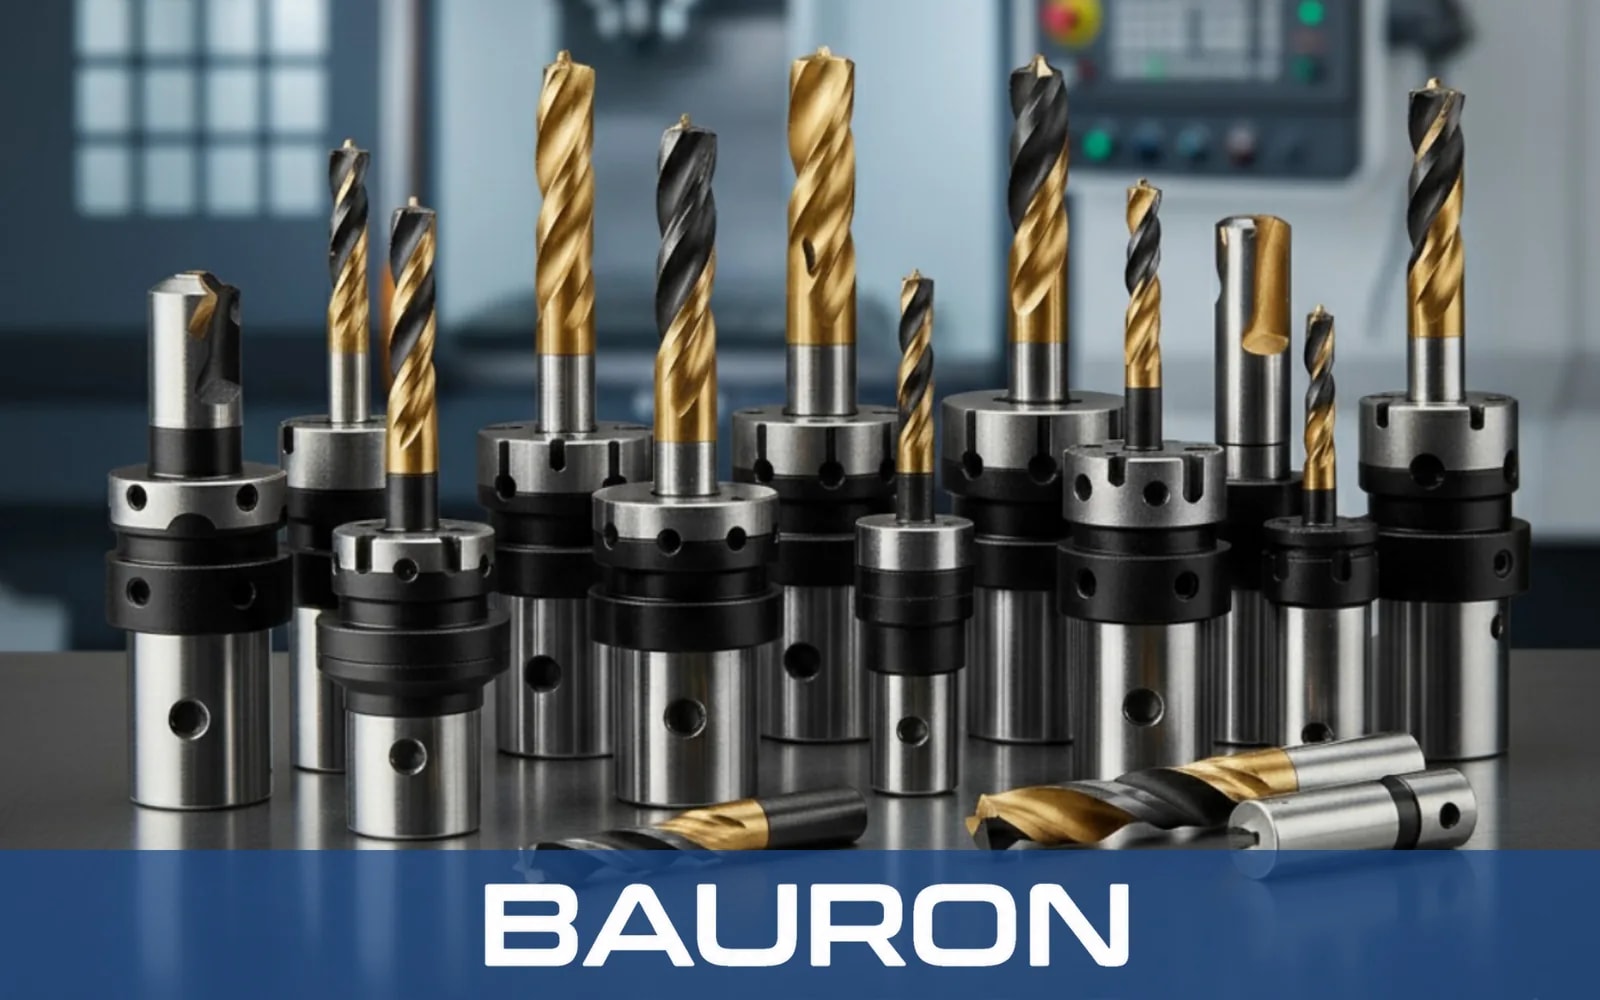
Sizes cylinder and valve-guide bores for automotive production.
Finishes rivet holes to specified dimensional tolerances.
Reams fluid passages to support close-fitting seals.
Adjustable machine reamers can be expanded to compensate for gradual cutting-edge wear.
Machines interference-fit bores for bearings in rotating assemblies across general manufacturing.
Hand reamers use square shanks and long entry tapers for slow manual turning. Machine reamers use round or tapered shanks for holder mounting and short lead chamfers for automated cutting.
Use an adjustable machine reamer when controlled expansion is needed to compensate for wear and maintain diameter across a production run.
Reaming friction generates heat. A compatible coating such as TiAlN can reduce friction and material buildup, improve the finished surface, and extend tool life.
No. A reamer follows the existing pre-drilled path and will finish an off-center pilot hole off-center. The centerline must be corrected with a boring operation before reaming.
Bauron can engineer straight, left-hand spiral, or right-hand spiral flutes for the workpiece material, machine, and chip-evacuation requirements, following the principles set out in the Reamers Design guide.
Bauron provides design and engineering support for custom machine-reamer profiles, flute geometries, coatings, shanks, and tolerances. Share the material, machine capabilities, and chip-control requirements for technical review.
Talk to Engineering