Flute Configuration
Straight flutes suit general through-holes and non-interrupted bores. Left-hand spiral flutes with a right-hand cut push chips forward and prevent the tool from catching over keyways or cross-holes.
This technical guide applies the core principles of tool design to reamer geometry, flute spacing, chamfer lead angles, and custom engineering for high-performance CNC reamers.
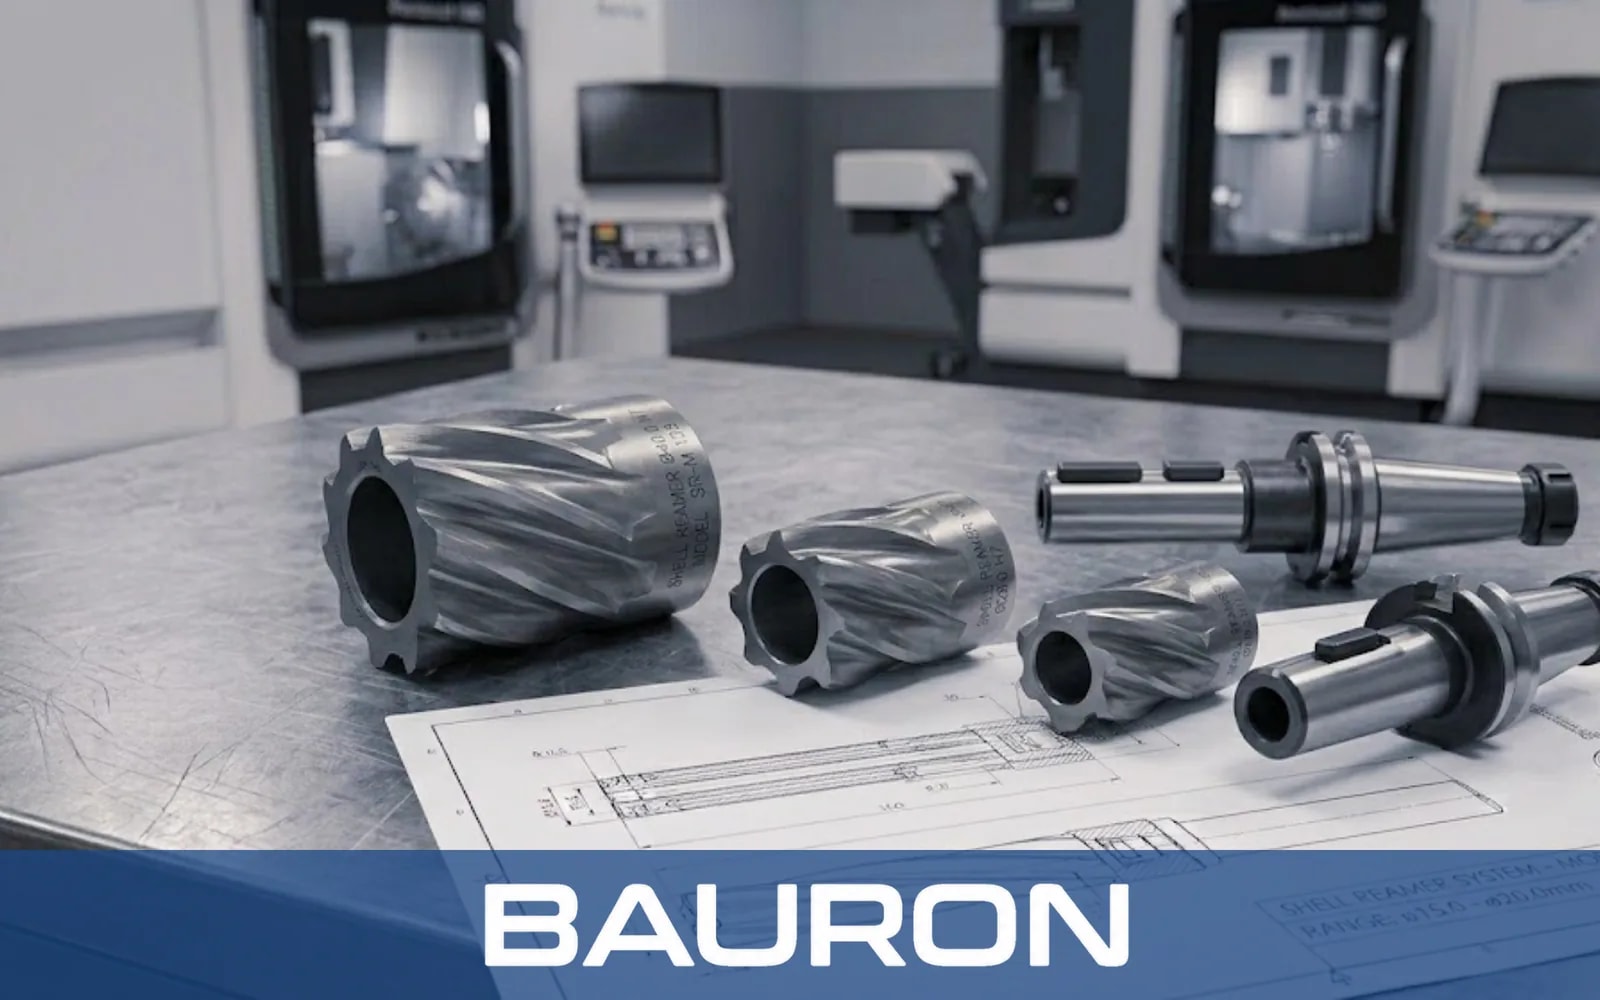
Optimizing reamer design is essential for precise hole roundness, strict dimensional tolerances of H7 or tighter, and mirror-like surface finishes. Reaming is a precision finishing process that removes thin layers of stock from pre-drilled holes. Effective custom reamers balance flute count, margin width, unequal indexing pitch, and chip-evacuation direction to prevent chatter and bore-sizing errors.
Straight flutes suit general through-holes and non-interrupted bores. Left-hand spiral flutes with a right-hand cut push chips forward and prevent the tool from catching over keyways or cross-holes.
Variable angular spacing between flutes disrupts harmonic resonance, eliminating chatter marks and supporting true roundness.
On a machine reamer, a 45° primary chamfer angle handles stock removal, while a secondary bevel or radius smooths the transition and supports high surface finishes.
Narrow circular margins reduce cutting friction along hole walls. A slight back taper prevents binding and scuffing during tool withdrawal.
Use sharp cutting margins, high positive rake angles, polished flute channels, and DLC or ZrN coatings to prevent material galling and edge buildup.
Solid micro-grain carbide substrates, left-hand spiral flutes, narrow margins, and heat-resistant AlTiN or nACo coatings support these demanding materials.
Straight flutes with negative rake preparation and ultra-fine micro-honed edges handle high hardness without tooth micro-chipping.
Diamond-coated PCD or micro-grain carbide reamers with high clearance angles resist rapid diameter wear, because these CNC tool materials hold their edge against abrasive fillers.
Standard reamers are limited to basic decimal sizes and standard tolerances. Specialized reamers built as custom cutting tools can address application-specific production requirements.
Combining bore sizing, chamfering, and face finishing in a single pass can shorten cycle times.
Custom reamers can be ground to exact sub-micron diameters, such as +0.0002 inch / −0.0000 inch, for specific bearing fits or dowel alignment pins.
Helical internal coolant delivery smoothly flushes micro-chips, extending tool life and preserving bore micro-finishes.
Bauron manufactures a complete range of reaming geometries, grouped by application. Each category diagram below is paired with the specific reamer types it contains.
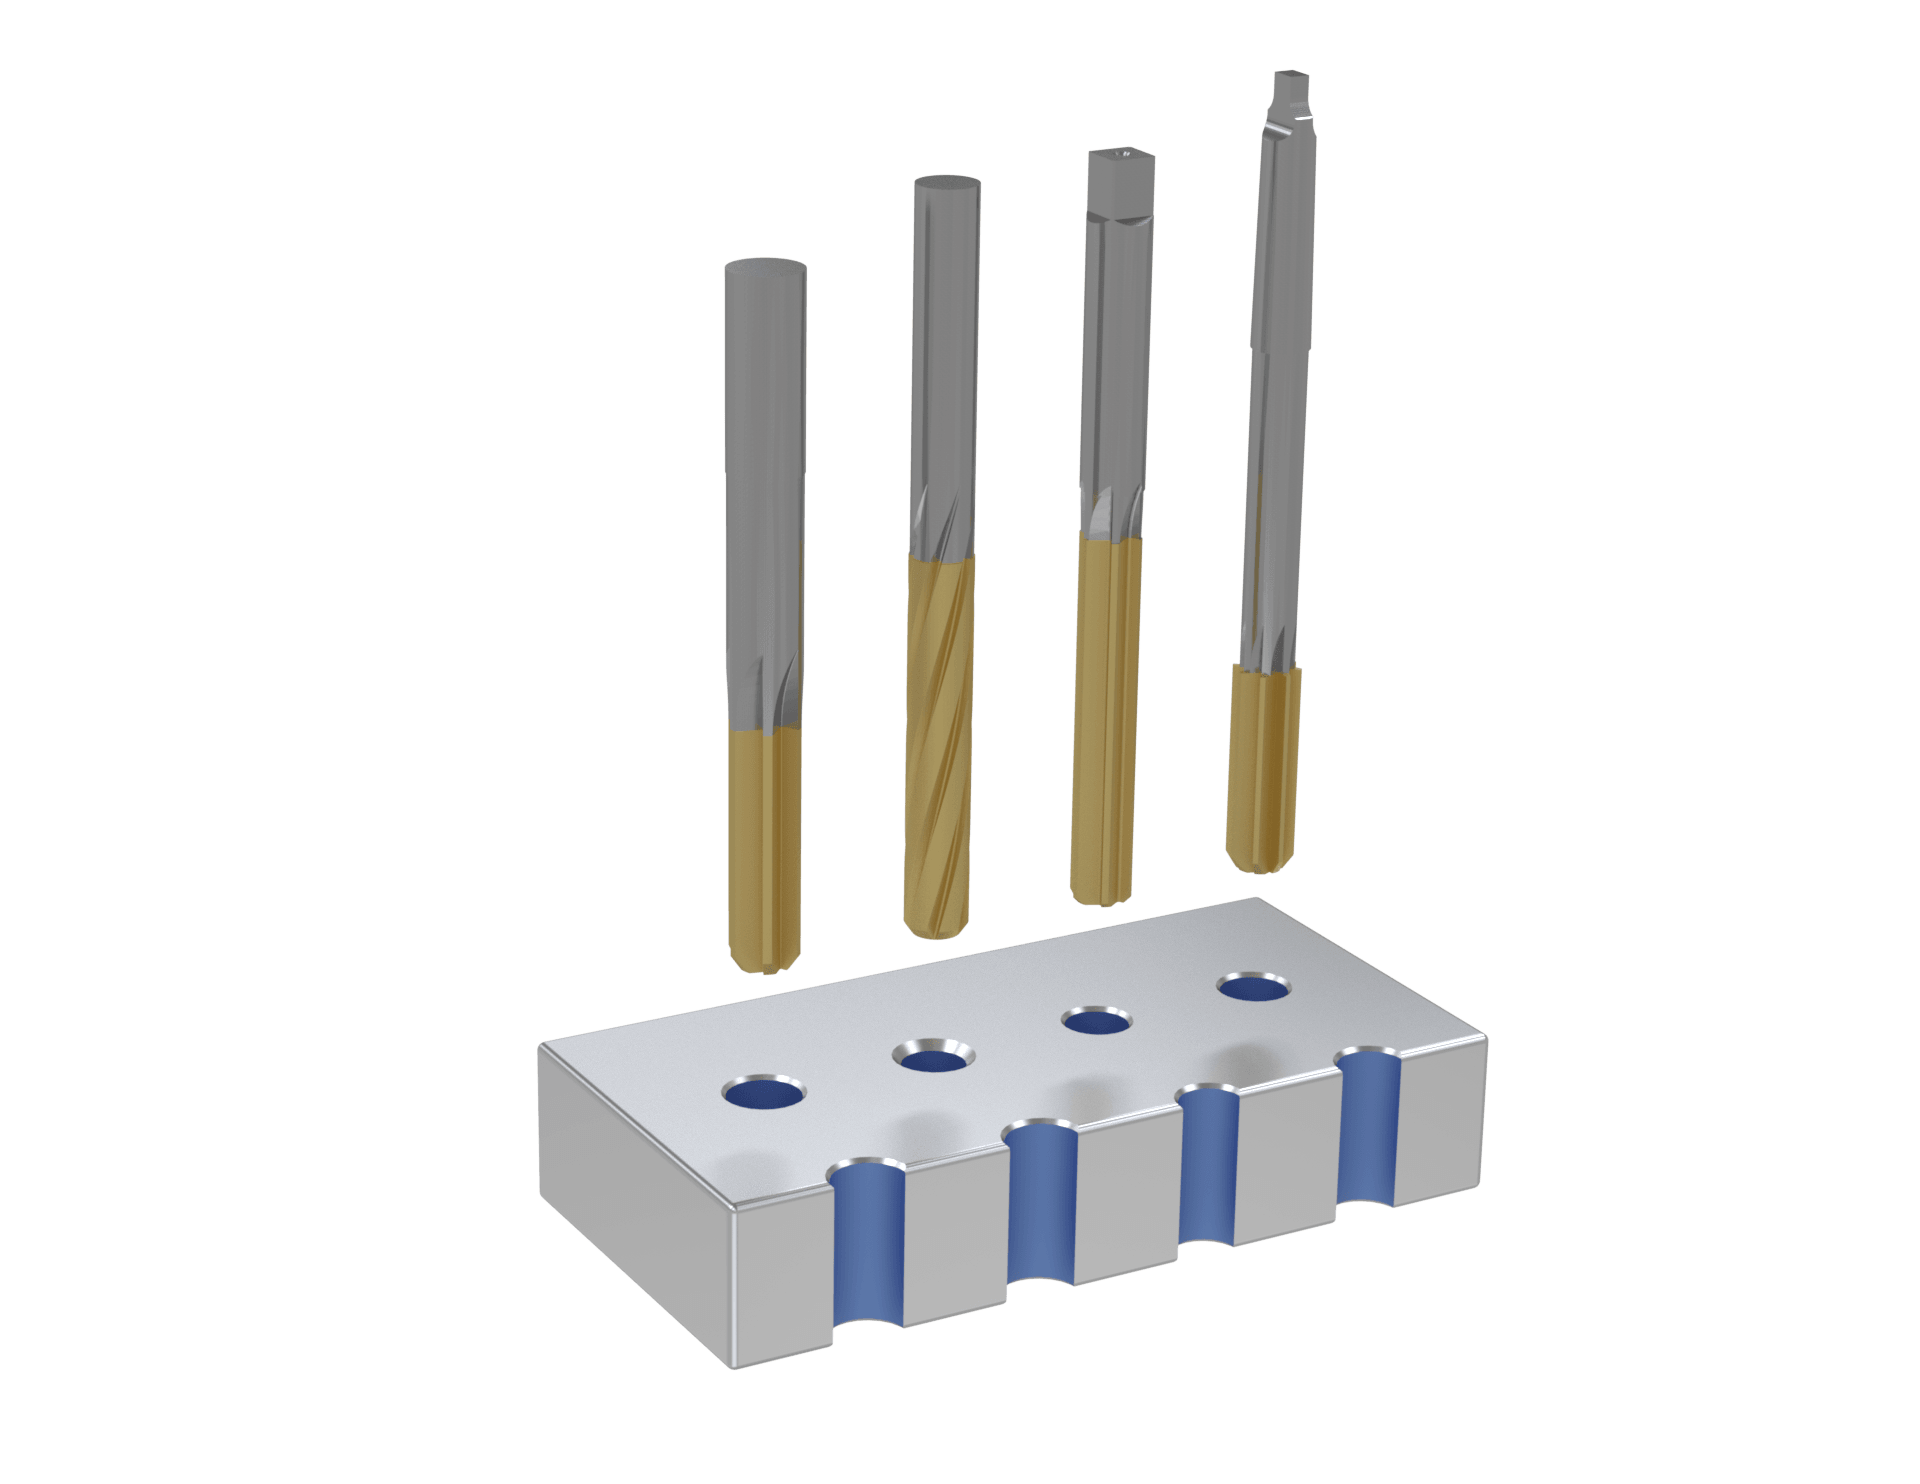
Accurate hole finishing for hand and machine reaming operations.
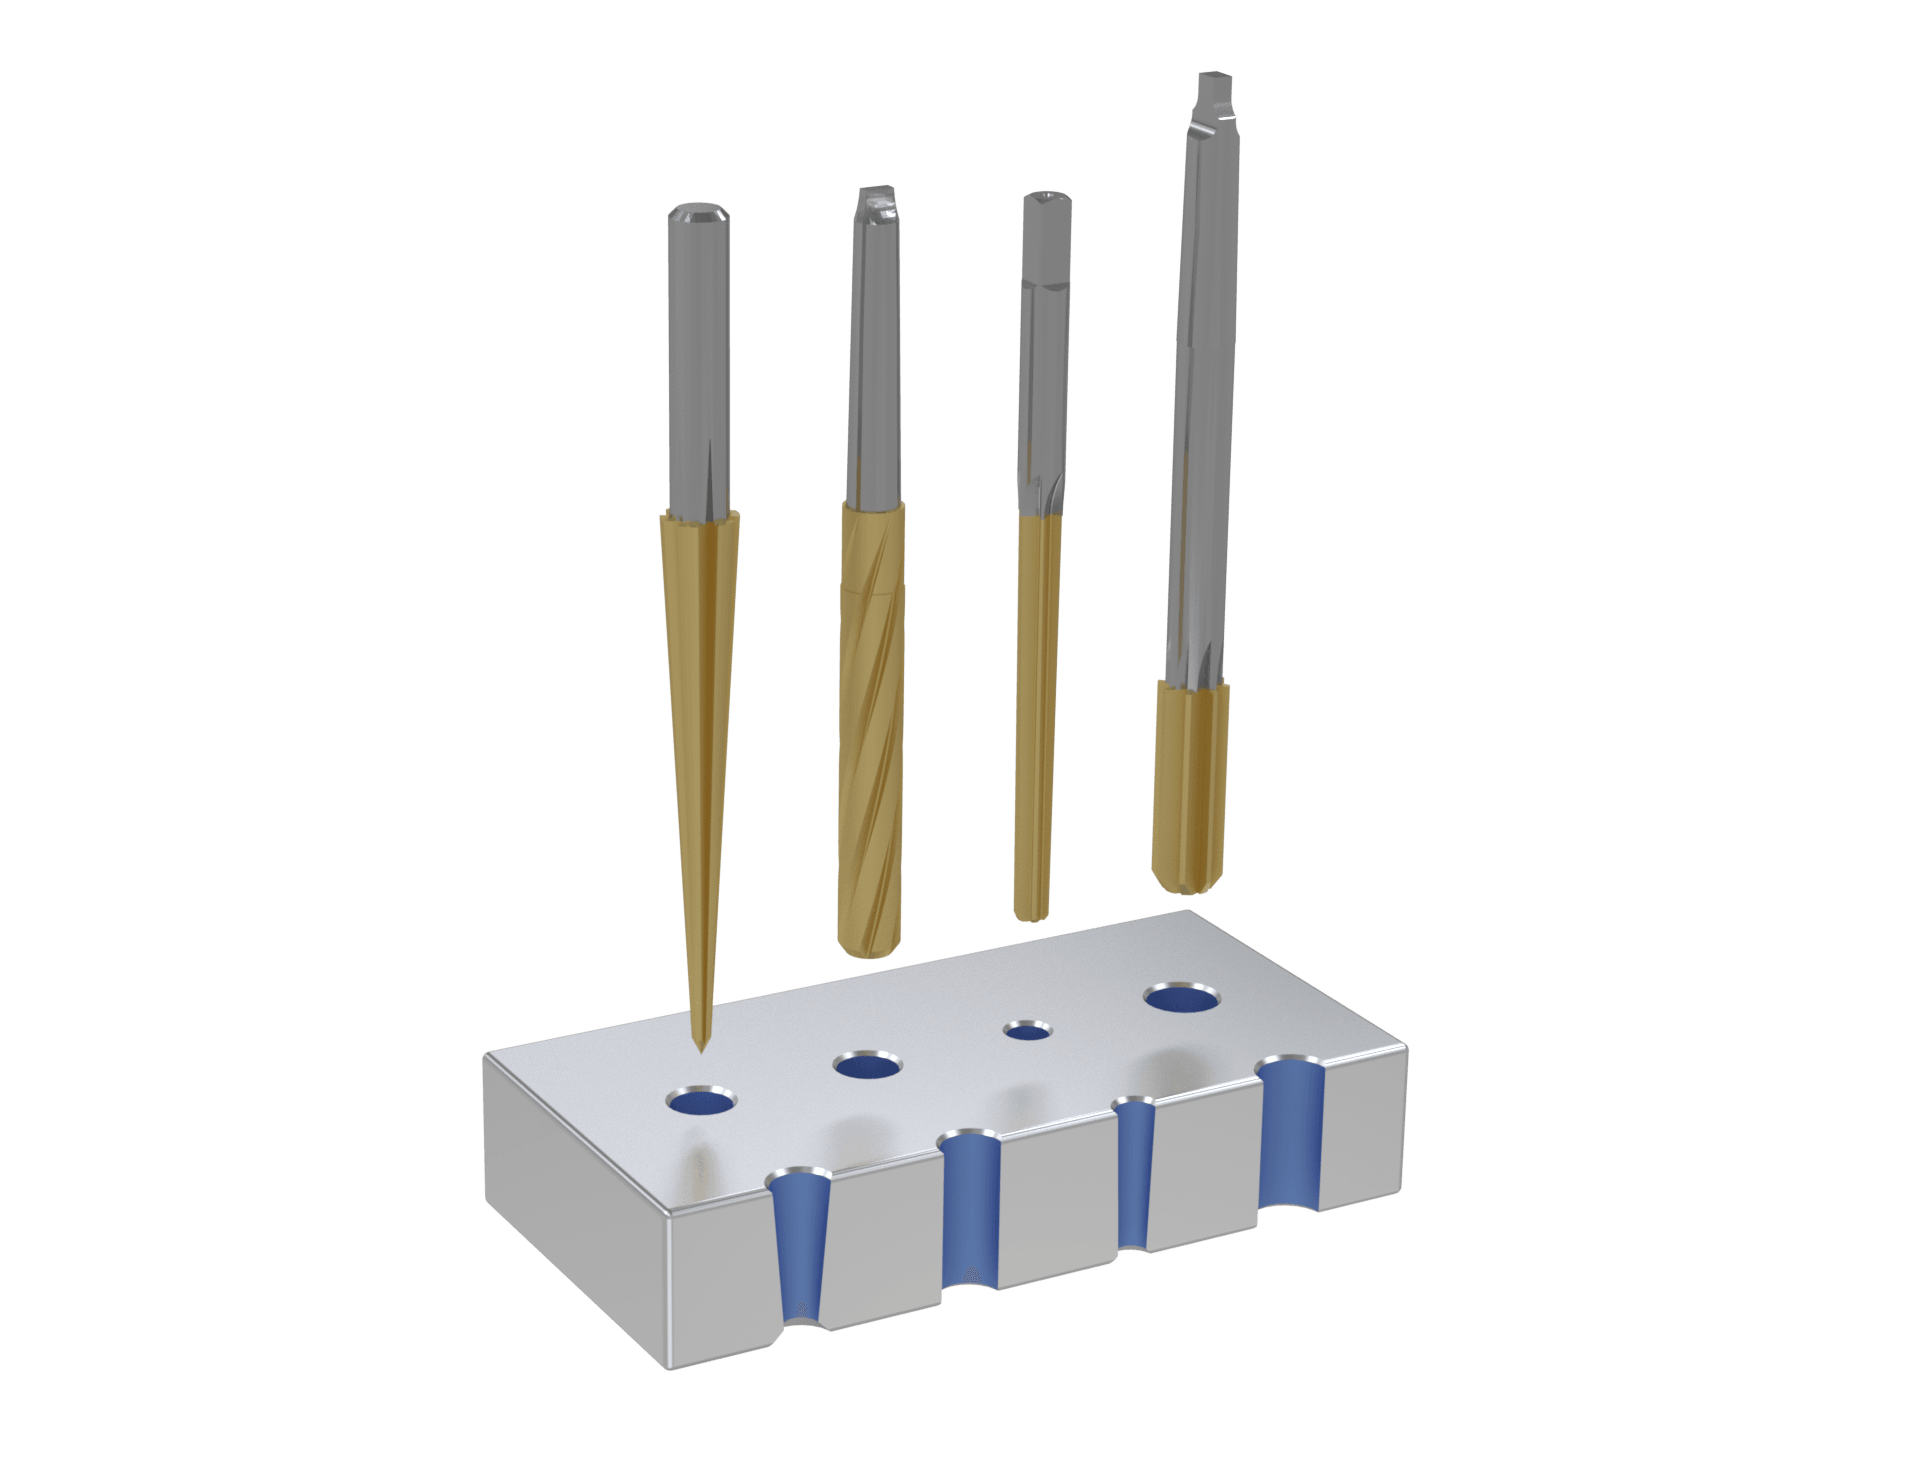
Precision geometries for tapered holes and tight-tolerance pins.
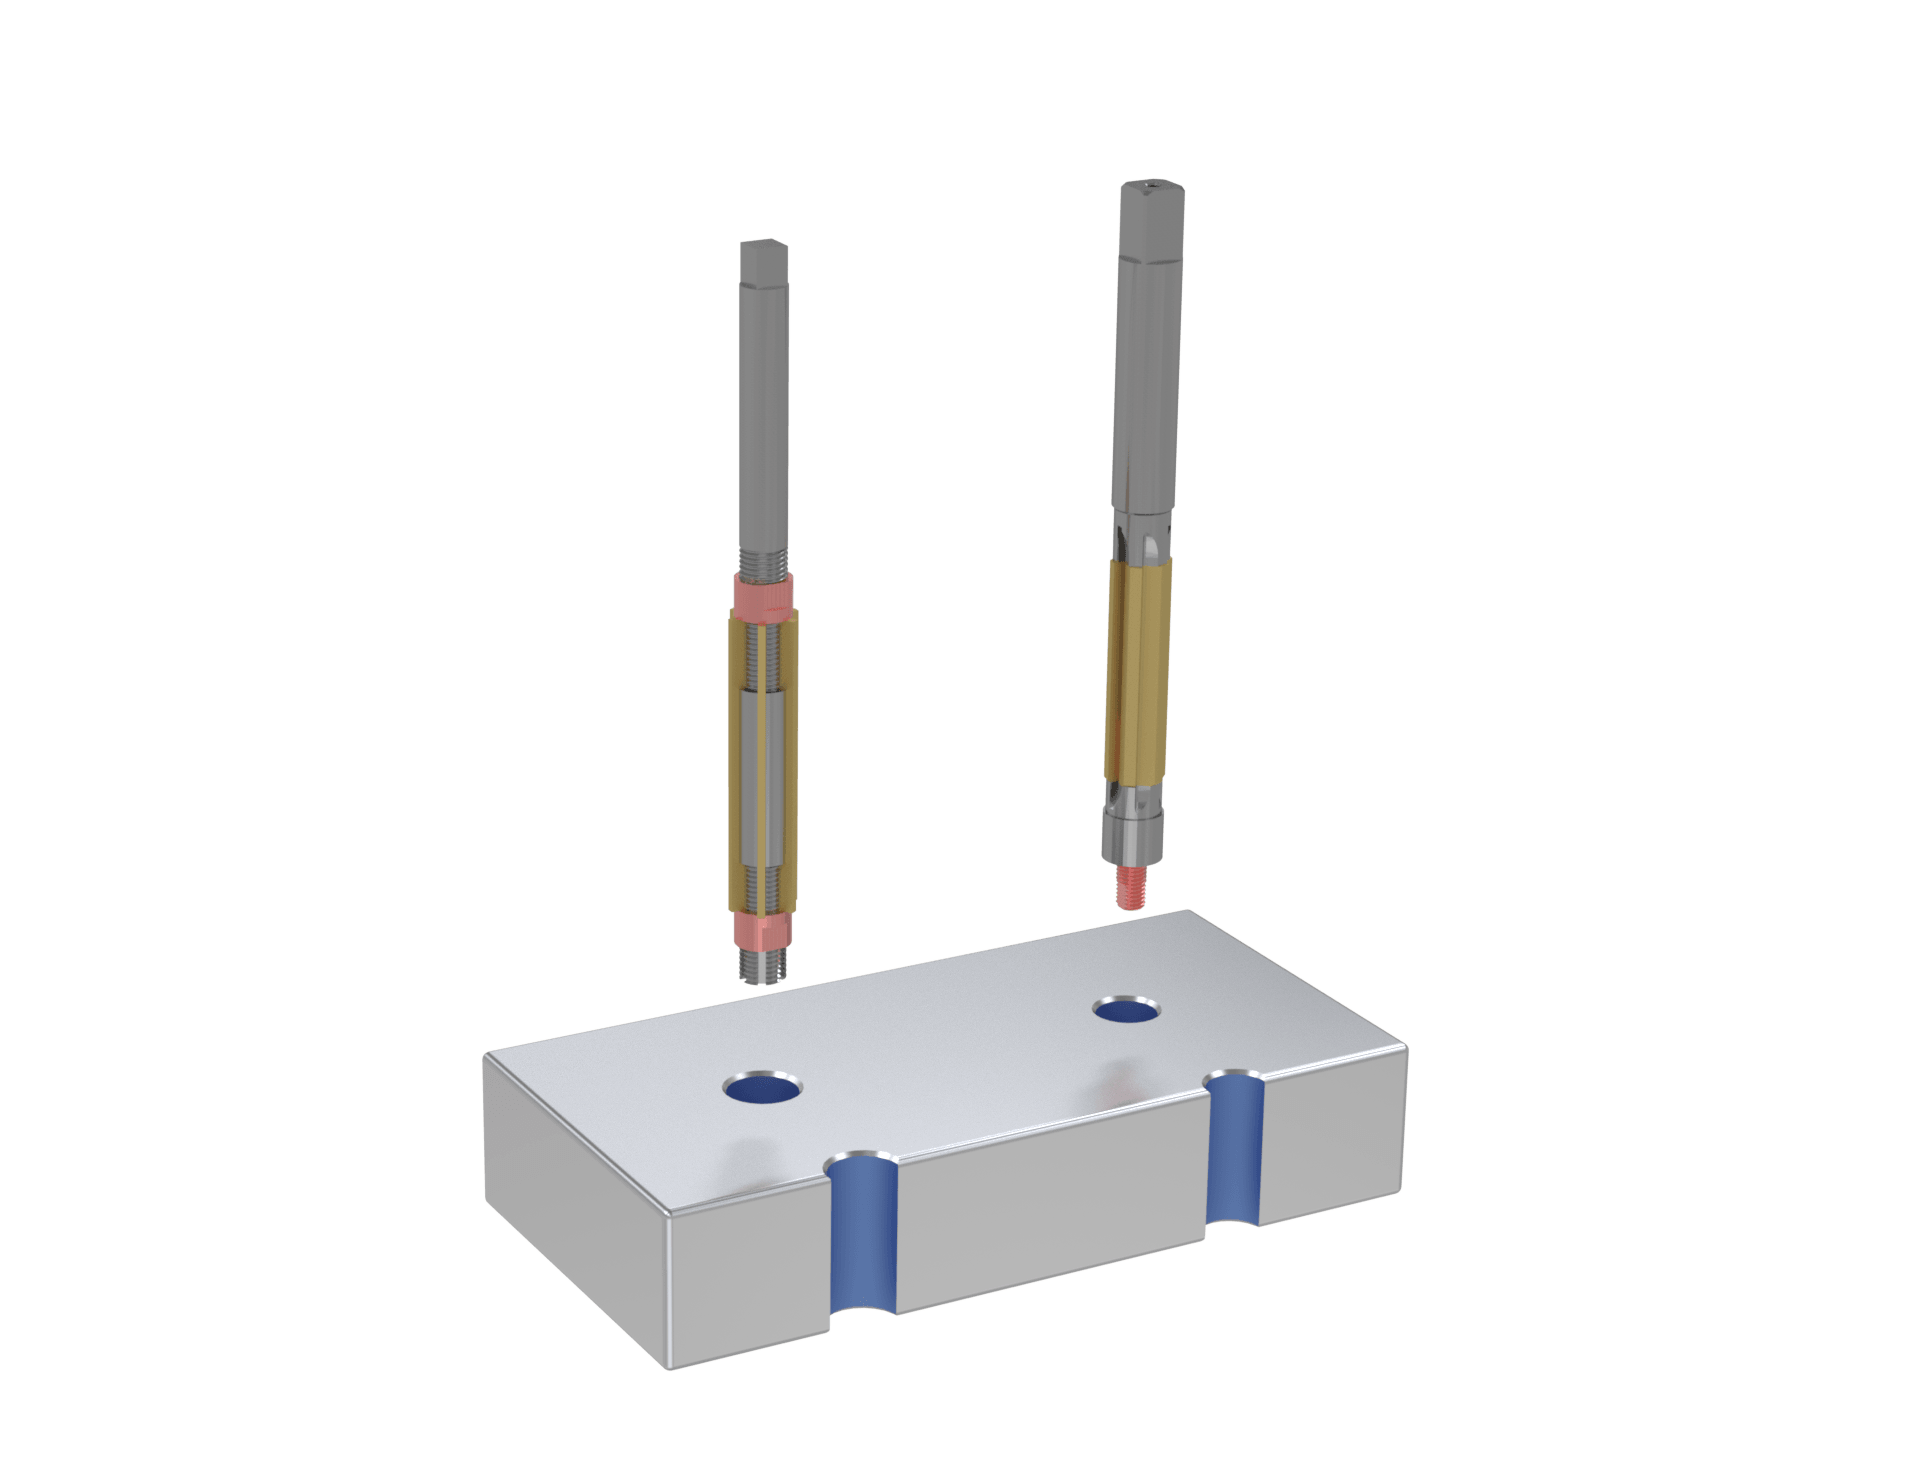
Diameter-flexible reamers for tight tolerances and worn holes.
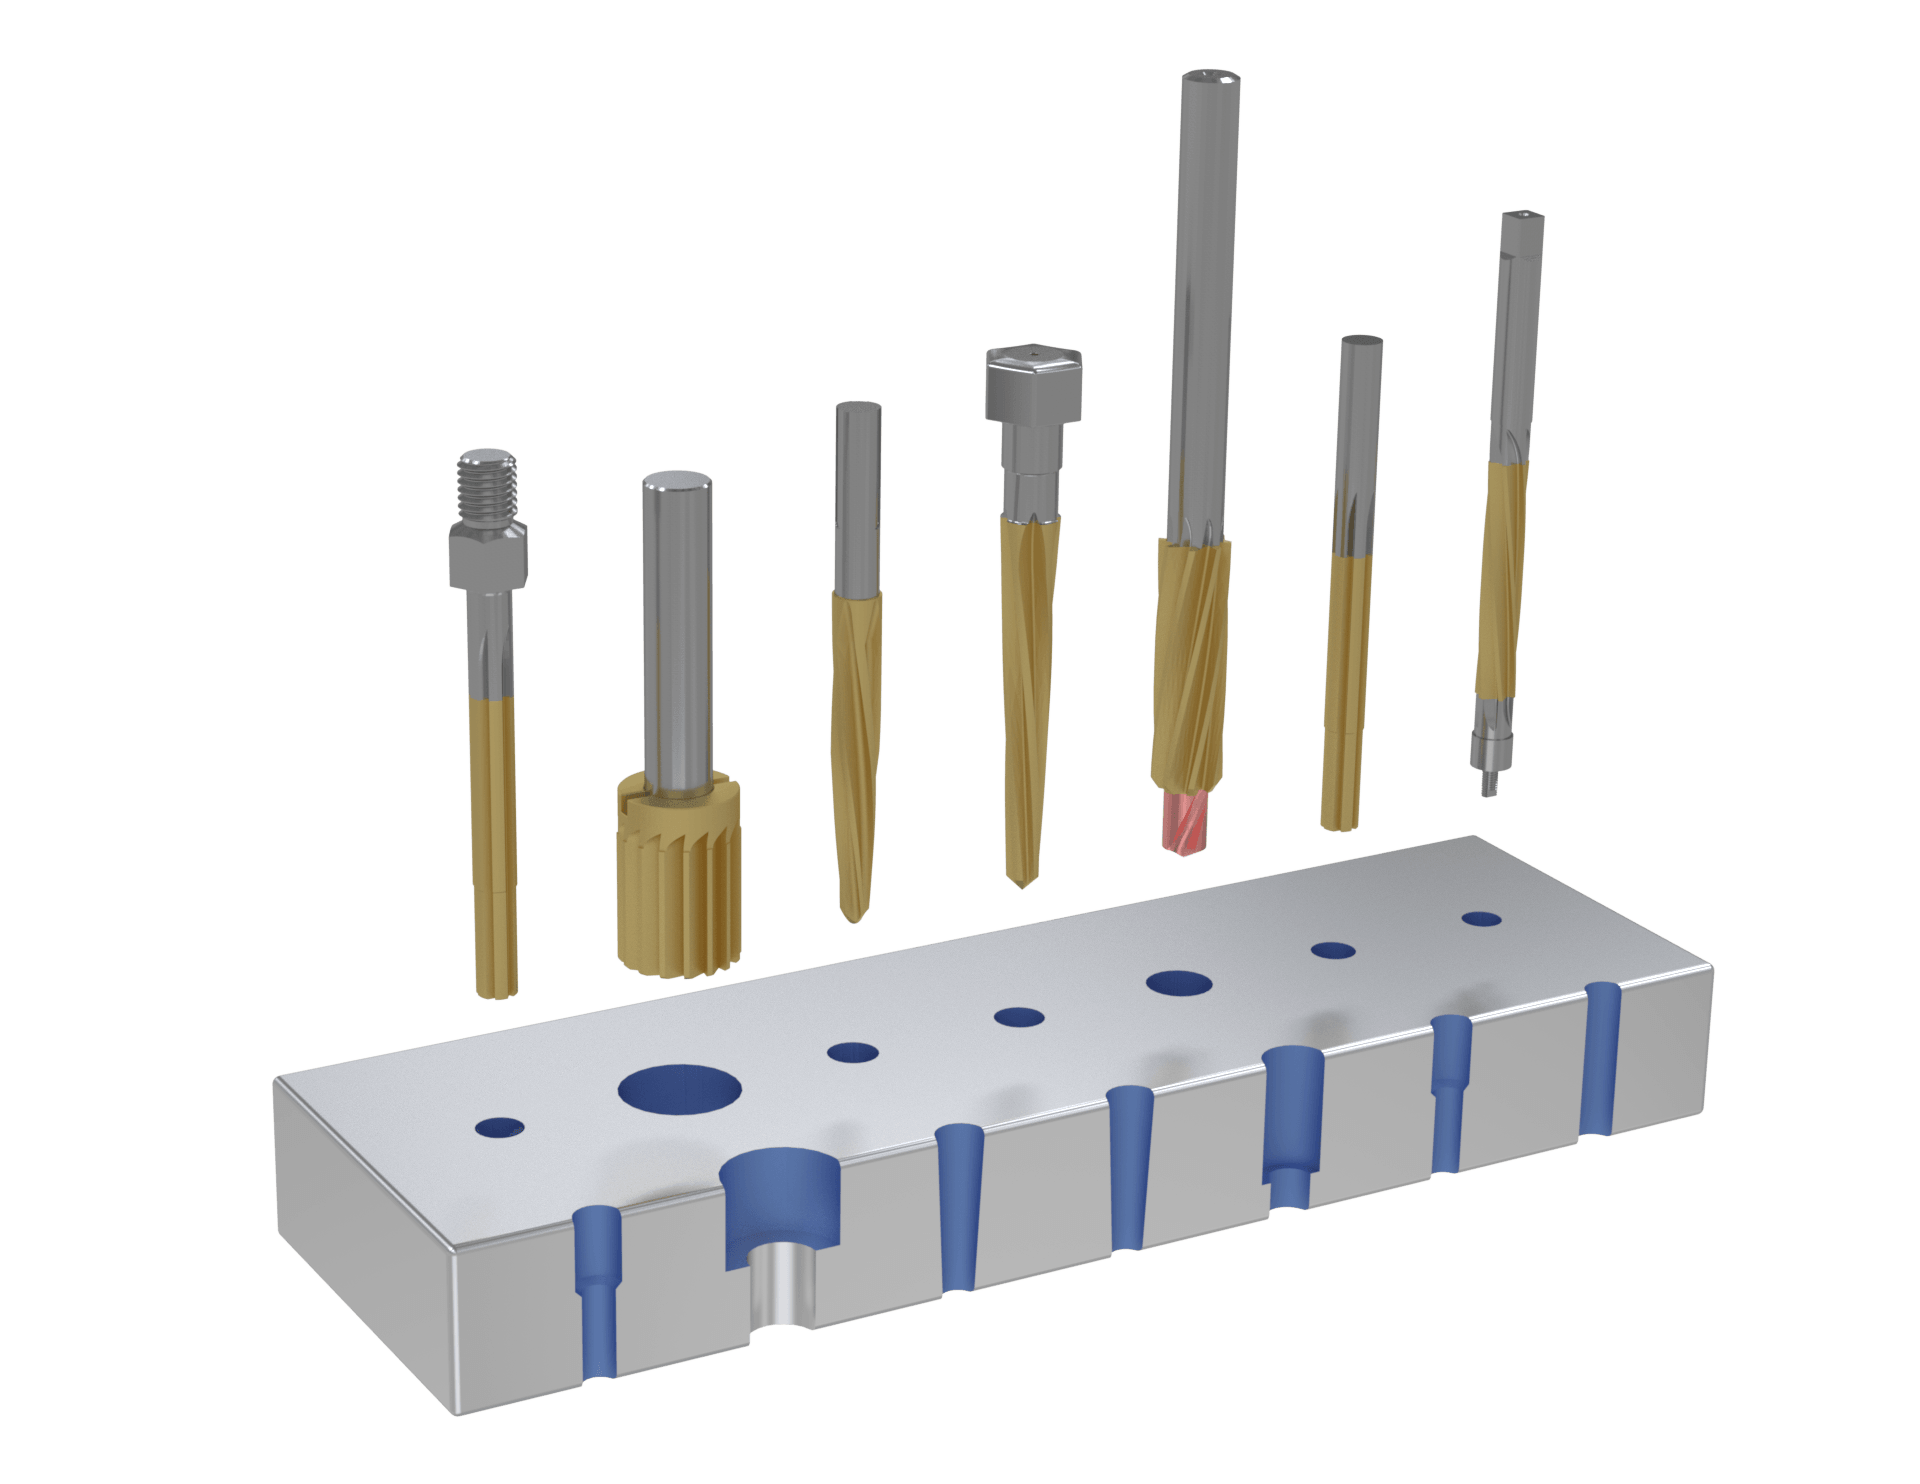
Purpose-built reamers for multi-diameter, structural, and industrial work.
Every Bauron reamer can be produced with the shank interface that best matches your machine and holder. Each shank type below is shown with how it mounts and where it performs best.
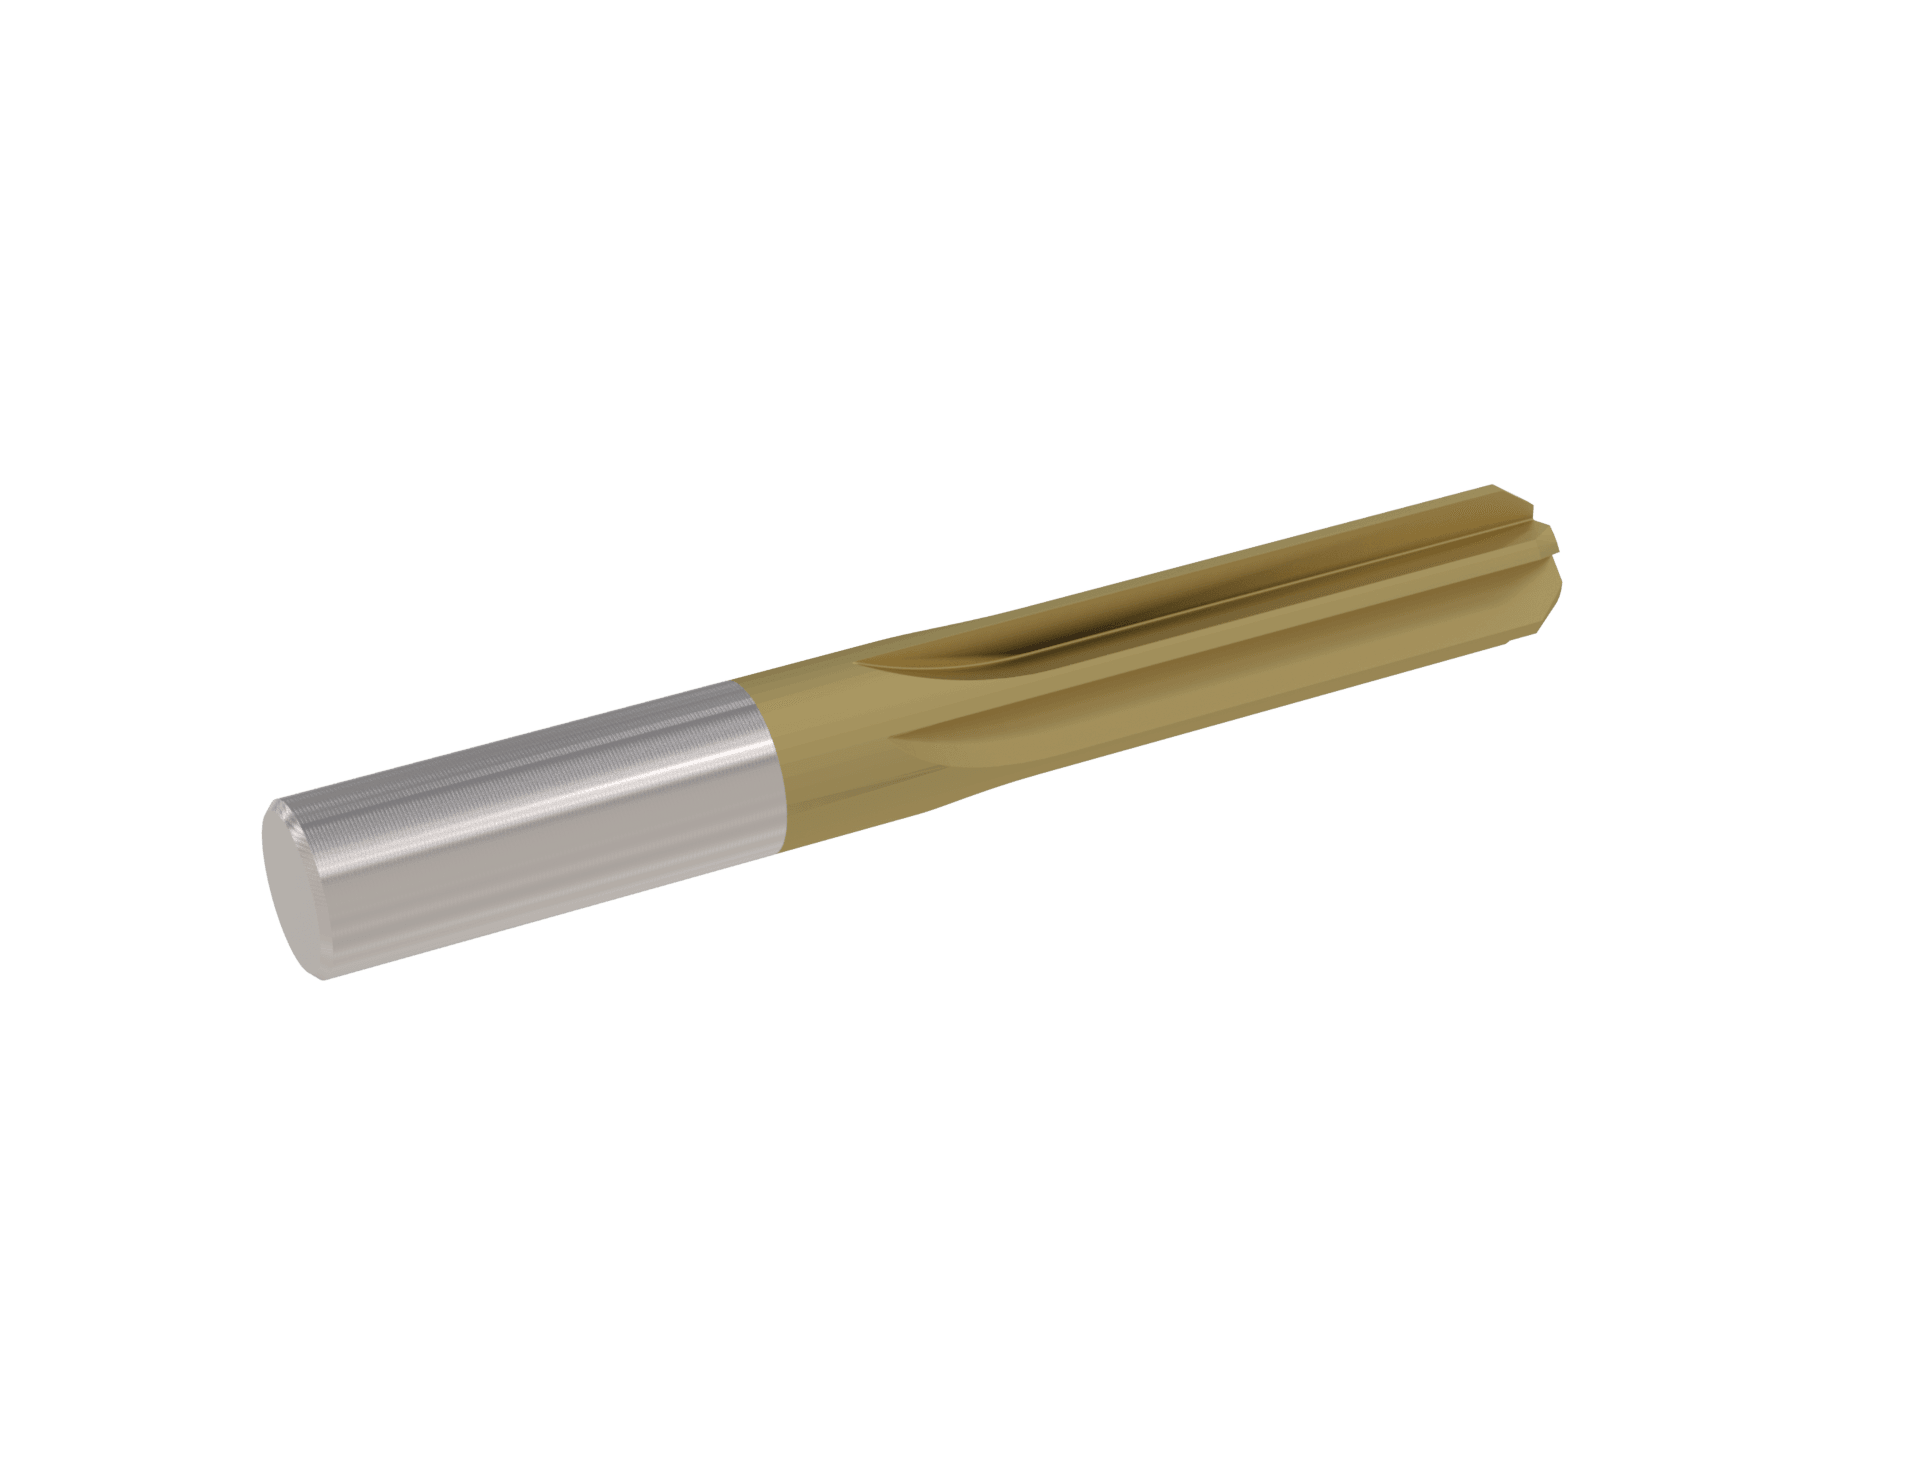
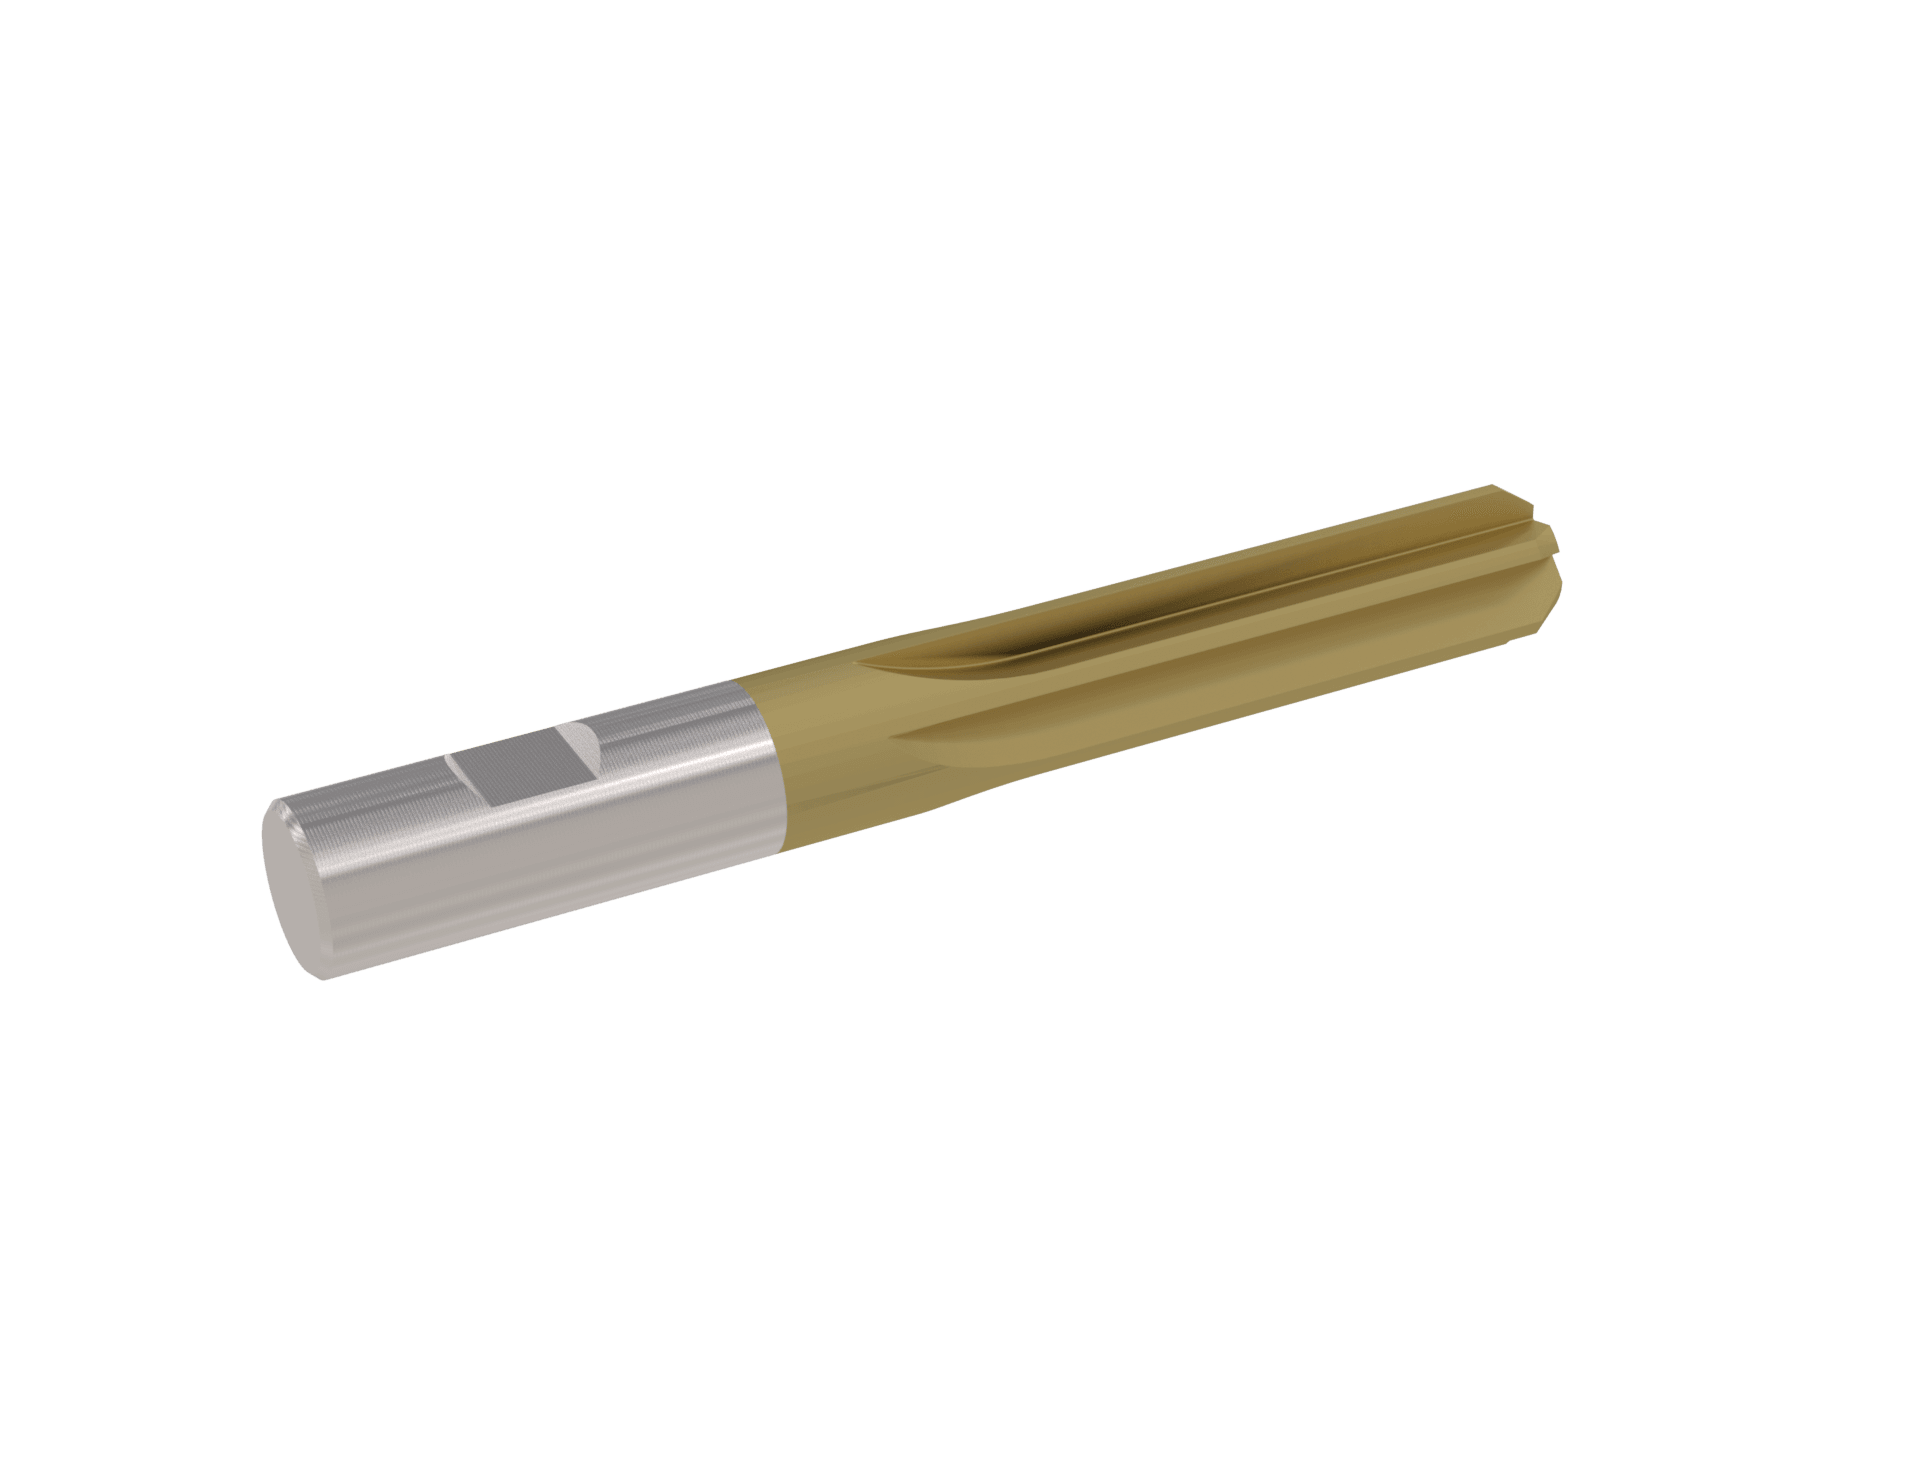
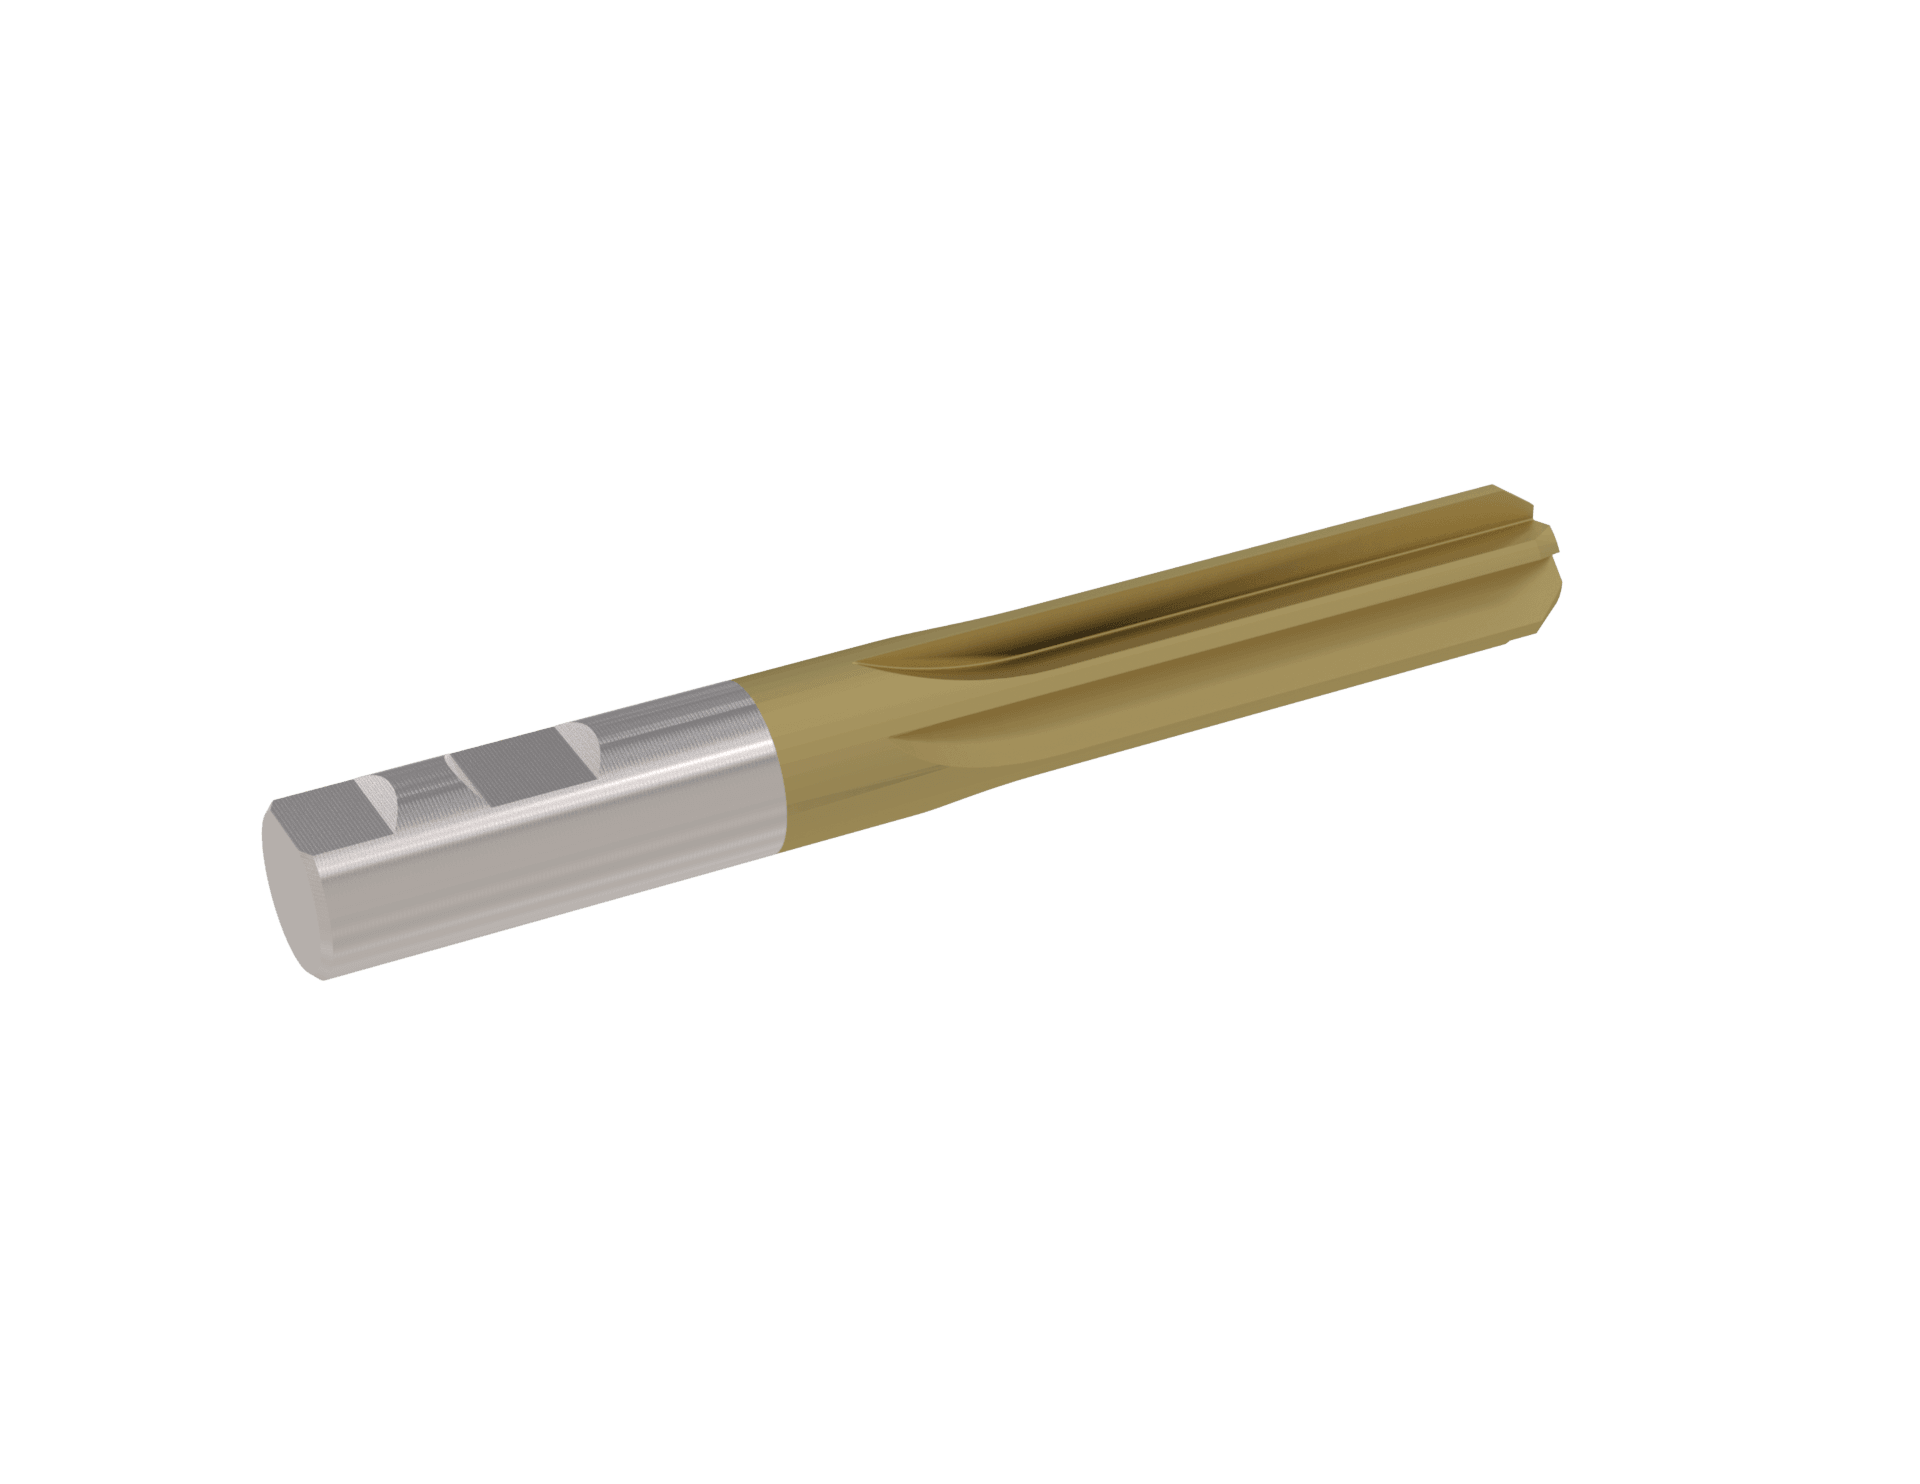
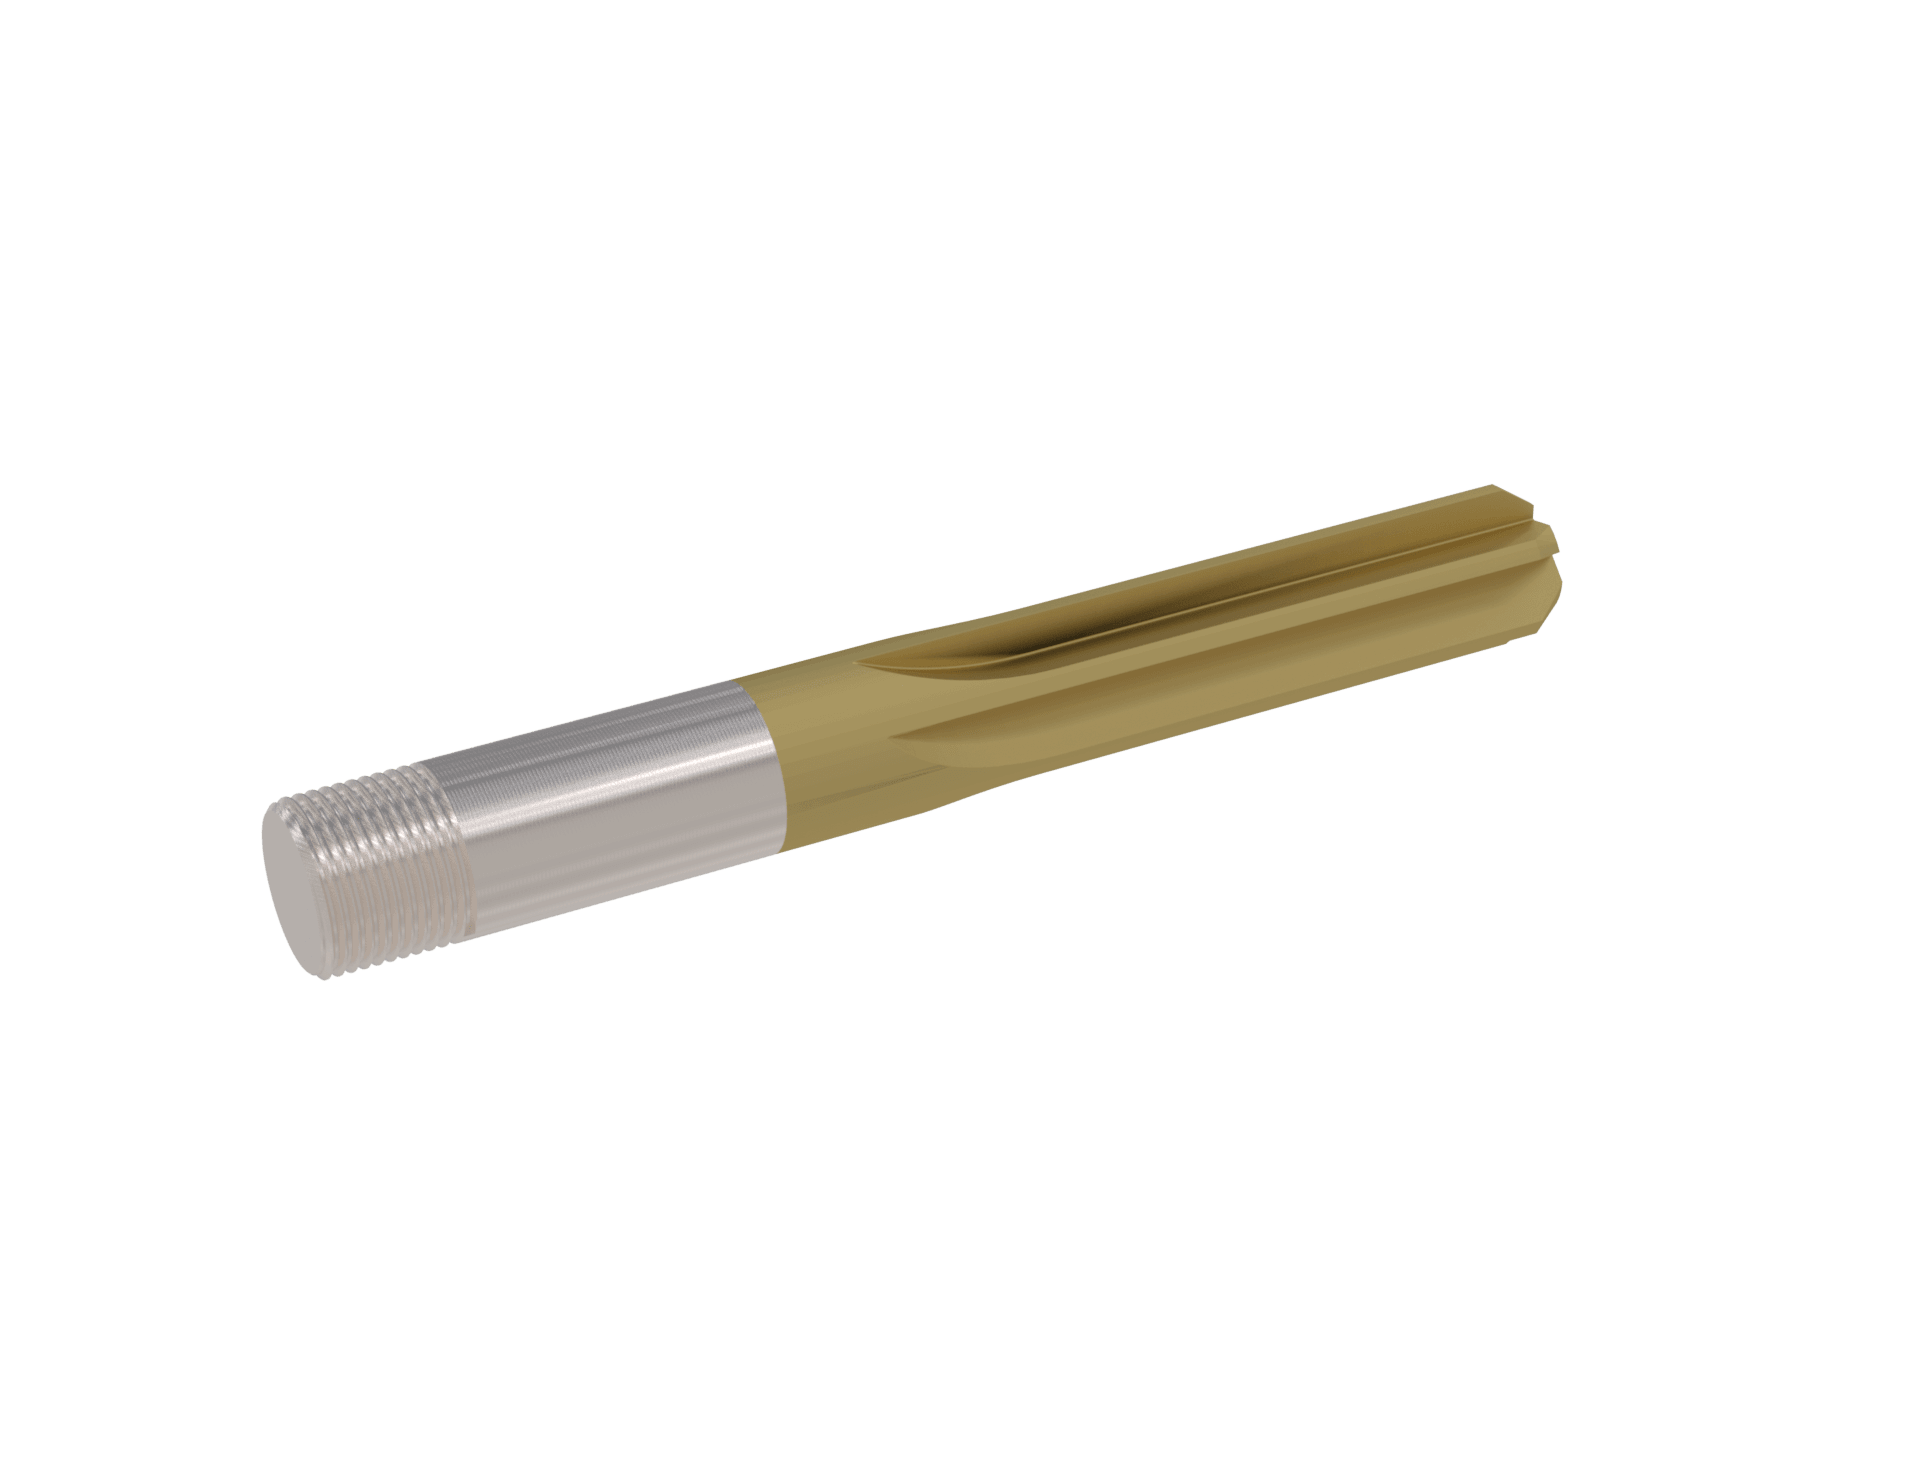
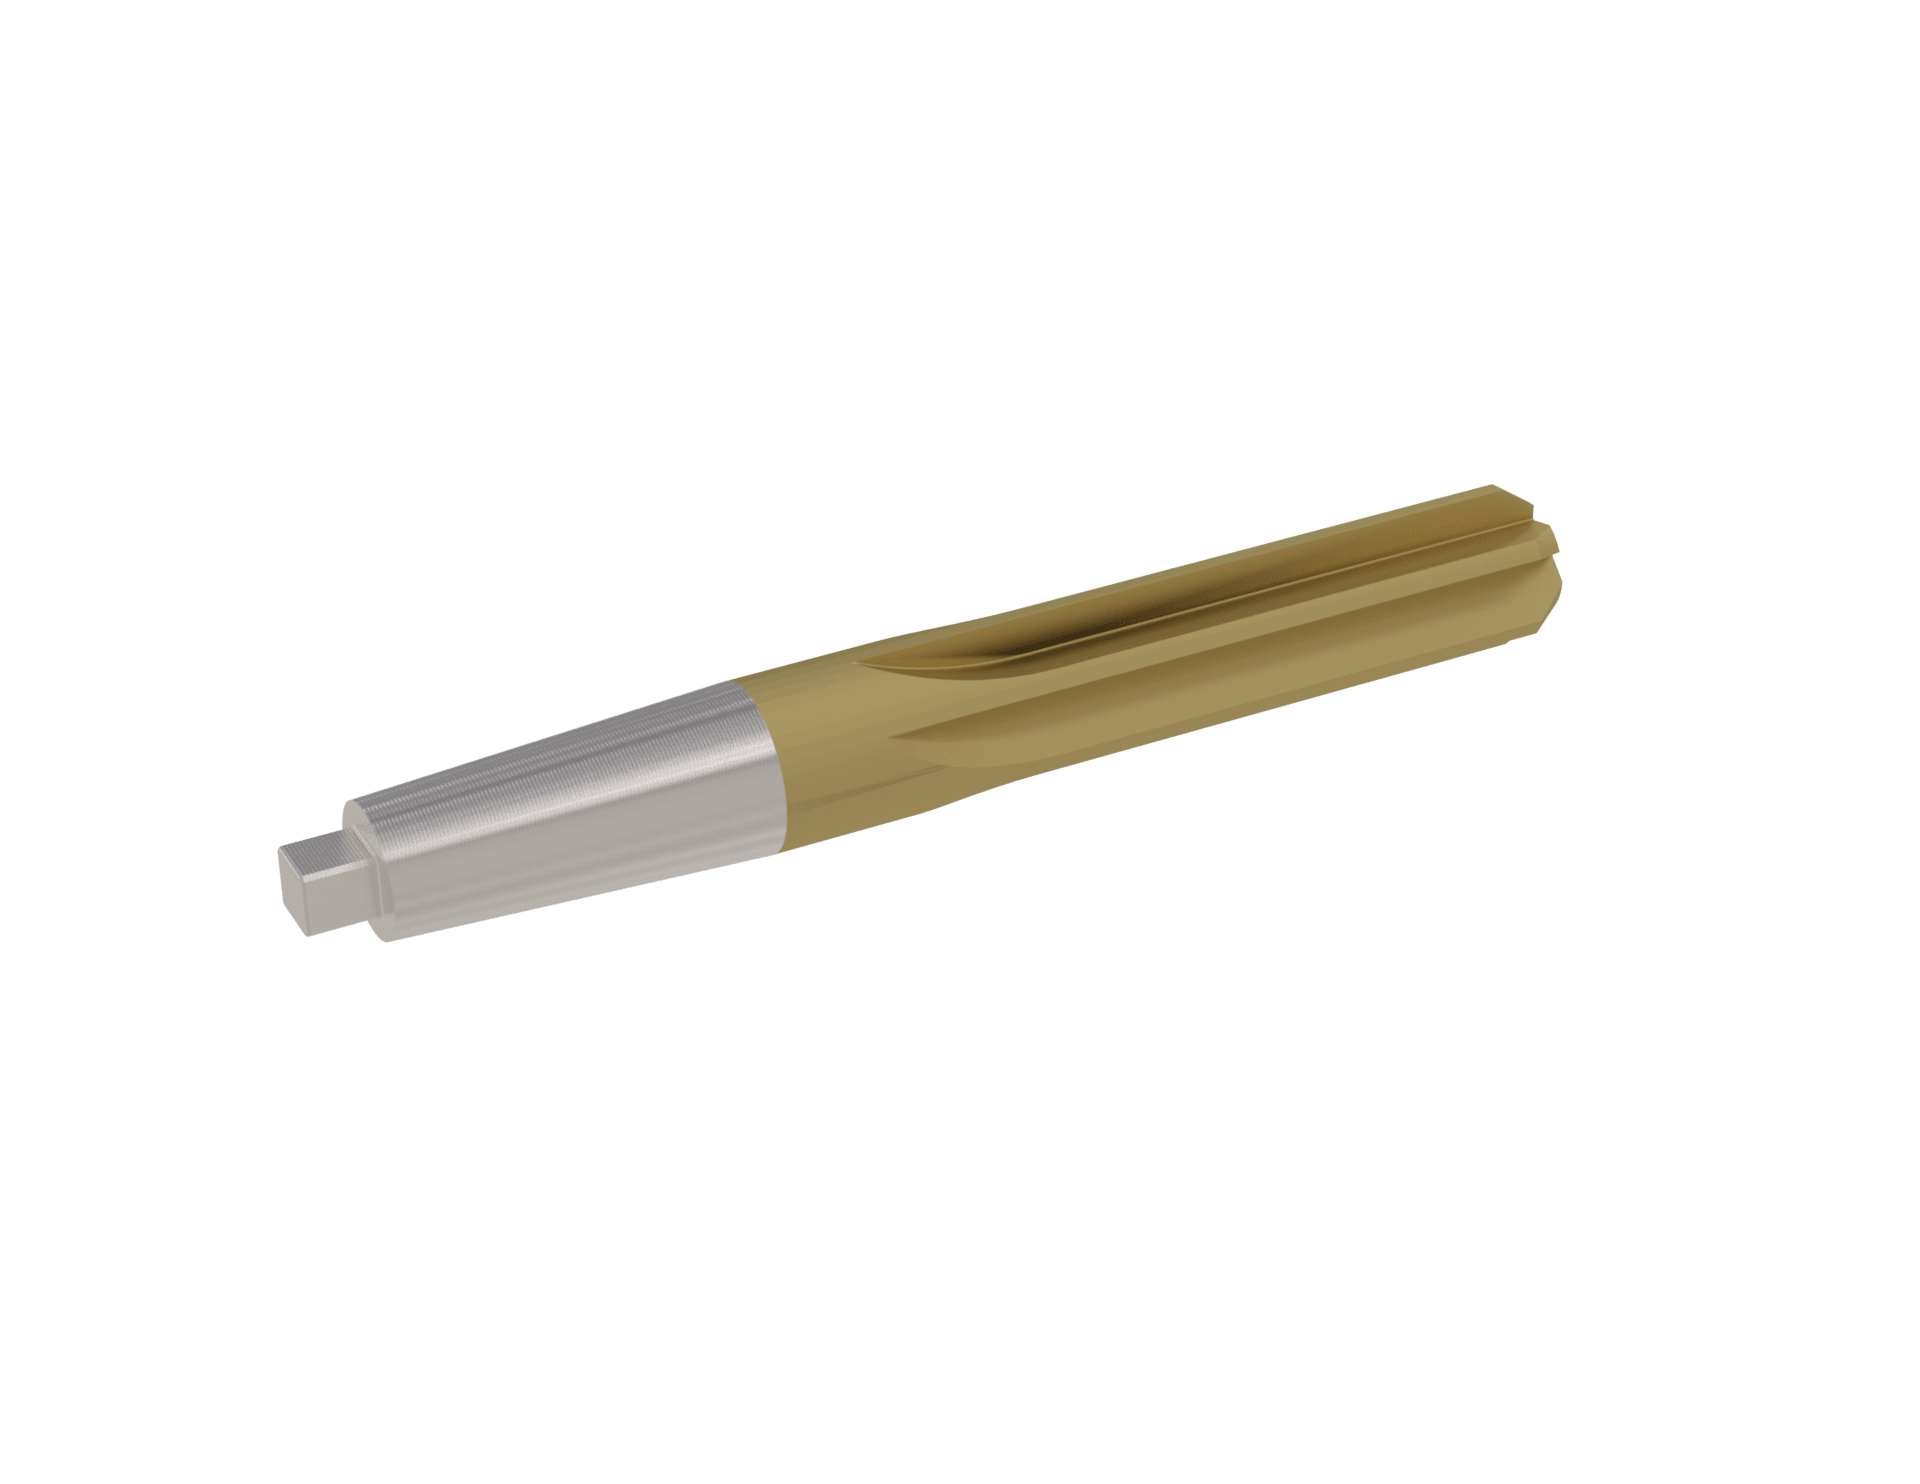
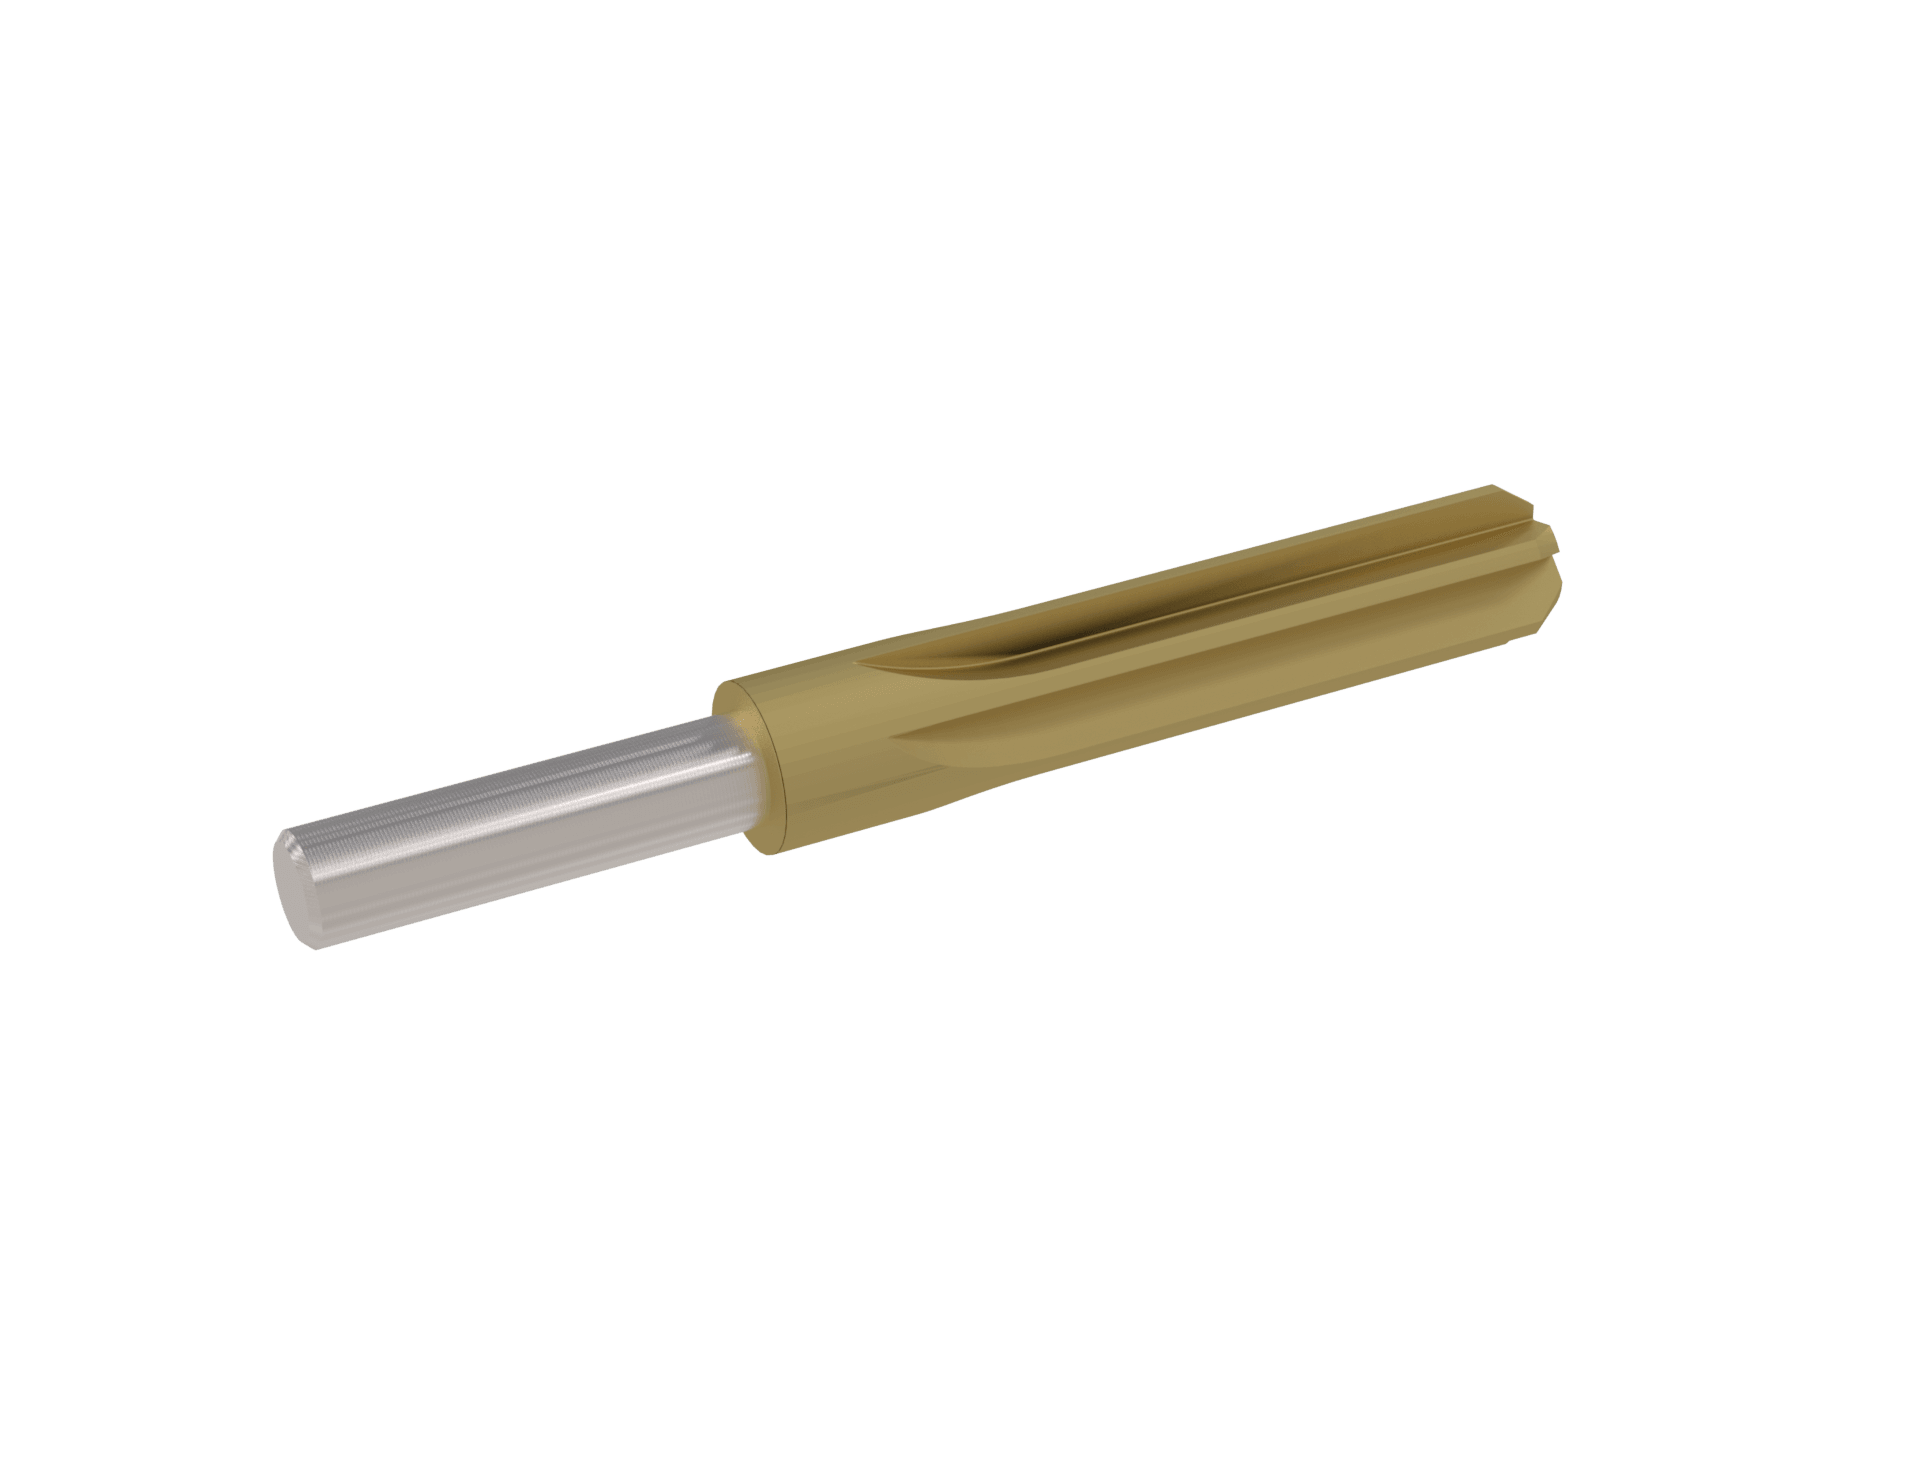
Unequal flute indexing disrupts harmonic cutting frequencies during high-speed rotation. This prevents chatter vibration and supports true circularity and smooth surface finishes in precision bores.
Custom reamers allow exact non-standard diameters, custom step transitions, unique chamfer angles, and specialized neck reaches tailored to workpiece material and blueprint callouts.
Yes. The engineering team at Bauron Precision Tools fabricates solid-carbide, HSS-Co, expansion, and step reamers directly from technical drawings.
AlTiN and nACo nanocomposite PVD coatings provide thermal stability and lubricity, protecting reamer cutting margins from heat and friction during titanium bore finishing.
The standards and reference documents behind the guidance on this page. Links open the publisher's site in a new tab.
Shows common reamer types and their geometric definitions, giving a shared vocabulary for reamer design features.
Establishes the ISO tolerance code system (for example H7) for holes and shafts: tolerance grades, fundamental deviations and fits.
Tables of limit deviations for standard hole and shaft tolerance classes, where the size limits of an H7 bore are read.
Specifies dimensions of machine chucking reamers with cylindrical shanks (1.32–20 mm) and Morse taper shanks (5.3–50 mm).
Specifies metric dimensions of hand taper pin reamers that produce holes for ISO 2339 taper pins from 0.6 to 50 mm.
Looking for high-precision CNC reamers, step-reamer geometries, or sub-micron hole-finishing solutions for your shop? Consult with a Bauron application engineer.
Bauron works with manufacturers to review tool geometry, substrate, coating, reach, machine conditions, and production requirements for standard and custom CNC tooling.
Submit your requirements