Deep-Cavity Clearance
The extended reduced neck enters a deep pre-milled cavity without rubbing upper walls.
Rotate the model with a mouse or one finger. Use the mouse wheel or a two-finger gesture for controlled zoom.
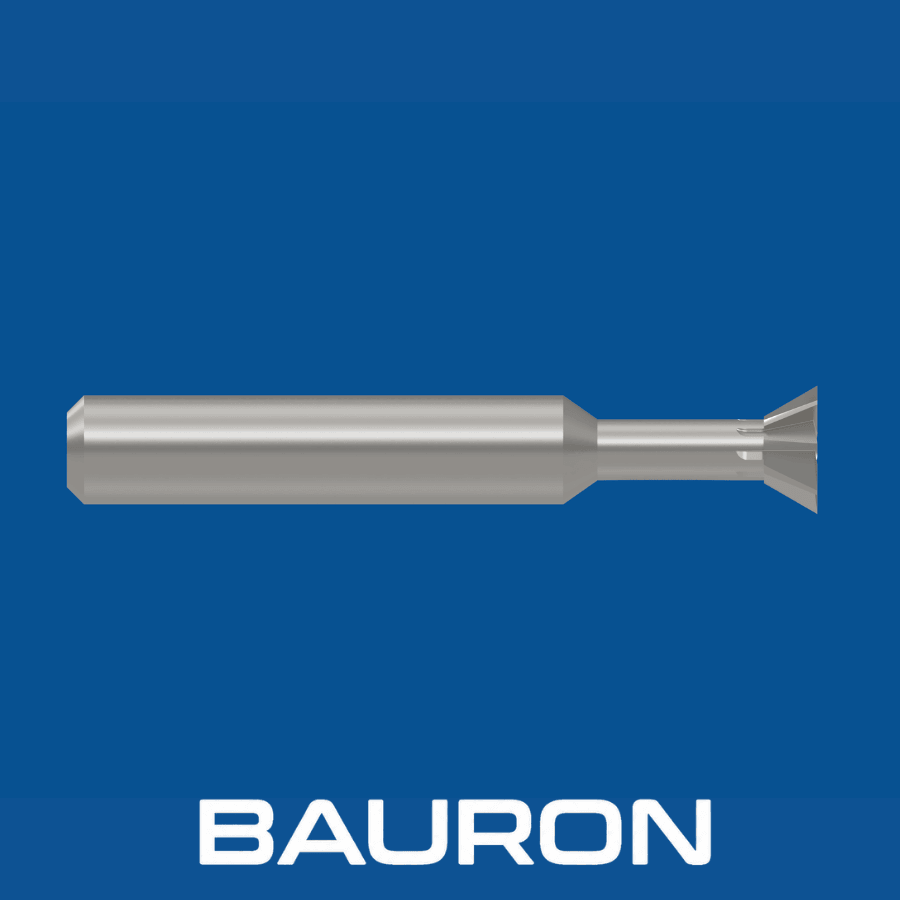
A long reach dovetail cutter is designed for deep-cavity undercuts. An extended reduced neck behind the flared cutting head reaches into tall-walled parts, recessed pockets, and housings where a standard shank or holder would interfere.
The extended reduced neck enters a deep pre-milled cavity without rubbing upper walls.
Flared teeth cut laterally into deep sidewalls to form 45° or 60° trapezoidal angles.
A tapered or thickened neck base helps limit chatter and deflection during long-overhang passes. For shallower slots under high cutting loads, a dovetail end mill with a blended neck radius is an alternative.
The ground cutting form produces deep sliding tracks for machine ways and workholding bases.
Clearance-neck options support undercutting at depths from 3 to 10 times the cutter diameter.
The long neck of the dovetail endmill keeps the shank, collet, and spindle nose above tall workpiece walls when properly specified.
A thickened or tapered base helps reduce flex and chatter during long-overhang side milling.
On these dovetail milling cutters, the cutting profile supports controlled trapezoidal slide angles and surface finish. Where a V-profile rather than a trapezoid is required, a double angle milling cutter cuts both flanks in one pass.
Flute spacing is selected to balance tooth count and chip evacuation inside deep cavities.
| Specification | Range / Details |
|---|---|
| Cutter Diameter Range | 3/8 in to 2 in+; metric 10 mm to 50 mm+ available |
| Included Angles | 45° and 60° standard; 30° and custom angles available |
| Reach Ratios | Extended neck clearance at 3x, 5x, 8x, and 10x cutter diameter |
| Flute Count | 4, 6, or 8 flutes |
| Shank Style | Straight cylindrical or Weldon flat shank |
| Operation Type | Deep-reach internal undercut slotting and trapezoidal slide milling |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| Solid Carbide | Stainless steel, titanium, hardened tool steels, and cast iron. | Stiffness helps reduce deflection and chatter during long-reach undercut passes. |
| TiAlN / AlTiN Coating | High-temperature alloy steels, titanium, and dry milling. | Thermal stability helps protect flutes from heat generated in deep pockets. |
| nACo / DLC Coating | Aluminum alloys, copper, and adhesive non-ferrous metals. | Low friction helps reduce material welding and chip packing in deep slots. |
Solid carbide provides stiffness for extended reach, TiAlN or AlTiN supports thermally demanding cuts, and nACo or DLC helps reduce friction in non-ferrous applications.
Reach deep, multi-angled cavities and complex recessed features.
Machine deep slideways in large industrial machine frames.
Use extended-reach toolpaths to finish deep internal slots with holder clearance.
Machines trapezoidal guide tracks and channels inside tall-walled valve bodies and housings.
Finishes deep internal dovetail slides on heavy machine-tool bases.
Prepares deep-set dovetail clamping features on tall structural components.
Cuts deep-reach trapezoidal joints in engine frames and housings, work Bauron supports as an aerospace tooling company for structural parts.
Compared with standard dovetail milling cutters, long reach models add an extended reduced neck behind the flared head so the cutter can access recessed slots without the shank or holder contacting surrounding walls.
Select a rigid cutter, use the shortest workable reach, reduce radial engagement, take light lateral passes, and clear chips with cutting fluid or air.
Yes. The flared head cannot plunge into solid stock. A rectangular relief slot must be cut first so the tool can enter and machine the angled sidewalls.
Choose the shortest neck that safely clears the deepest feature. Excess reach increases leverage, deflection, and cutting-edge load. If no standard length fits, the neck can be specified to the part, as with other custom milling cutters.
Bauron can review custom neck lengths, neck tapers, included angles, and coating requirements from part drawings.
Bauron provides design and engineering support for custom geometries and coating selections, and long-reach dovetail forms can be produced as custom carbide tooling. Share the slot depth, profile, material, tolerances, machine, and production requirements for technical review.
Talk to Engineering